


 English
 русский
 Deutsch

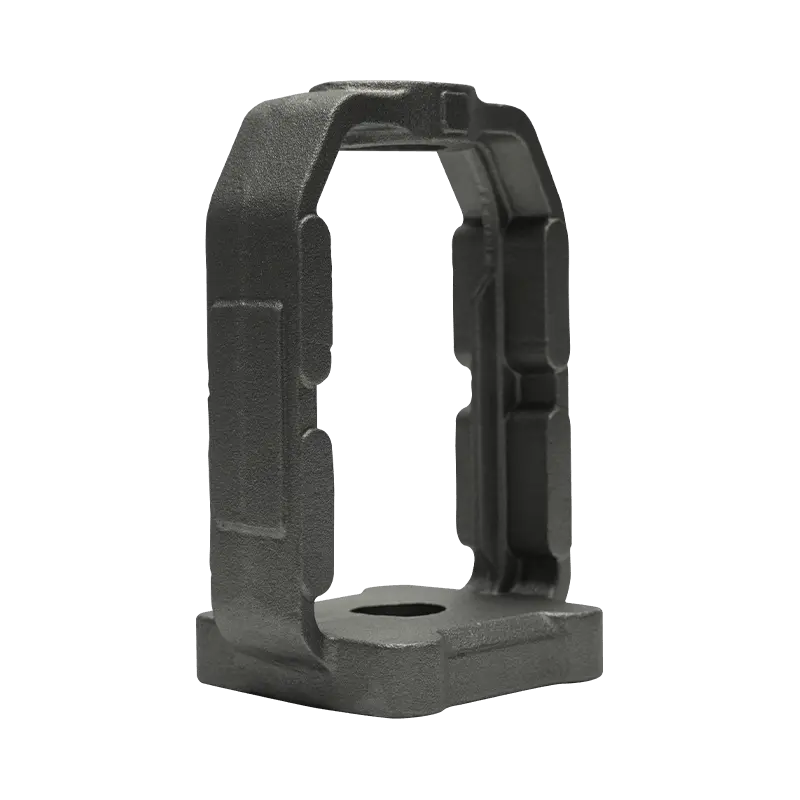
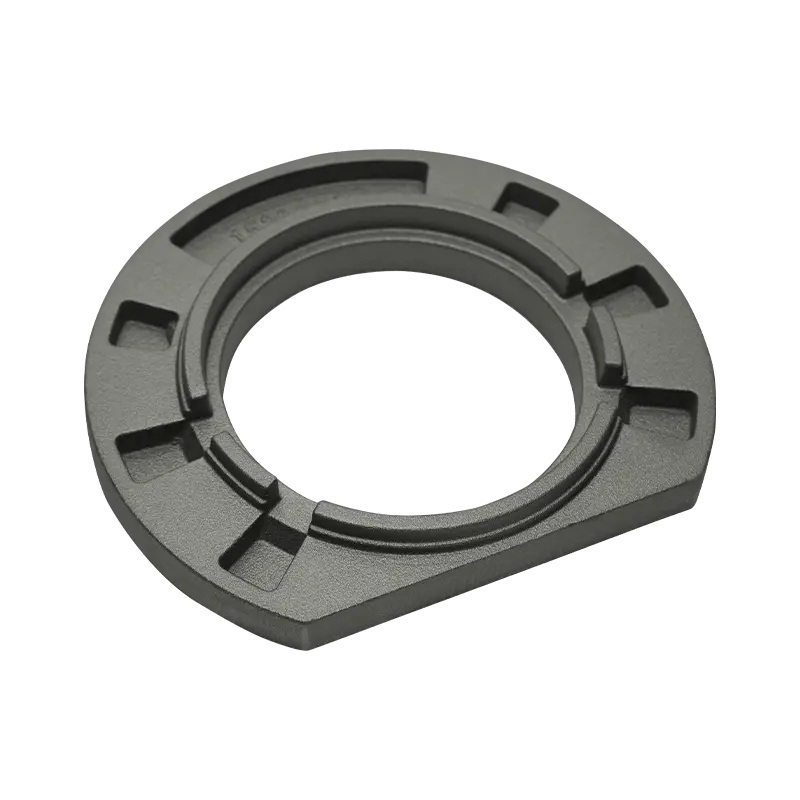
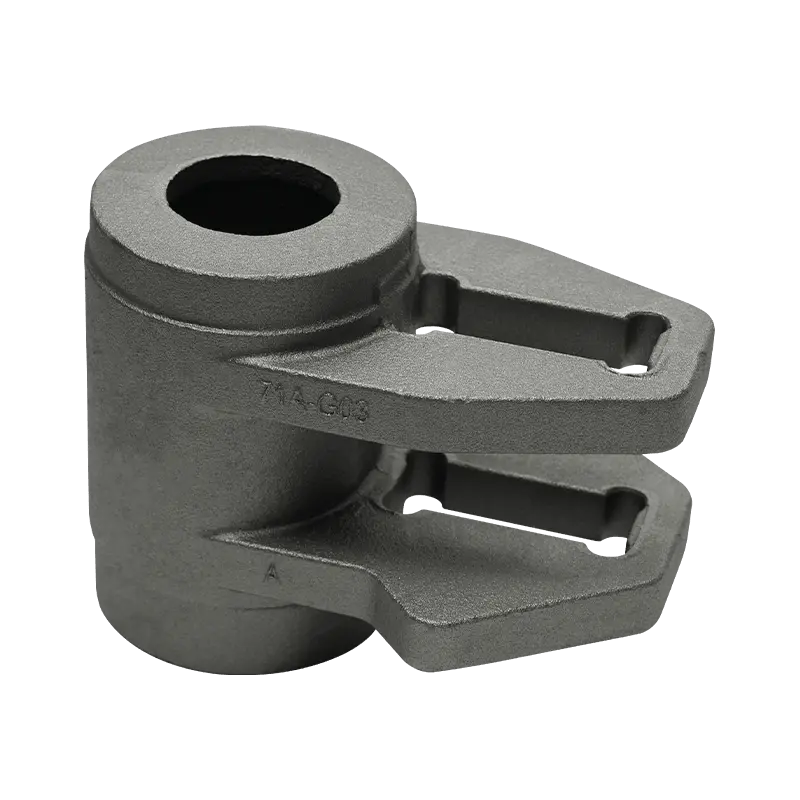
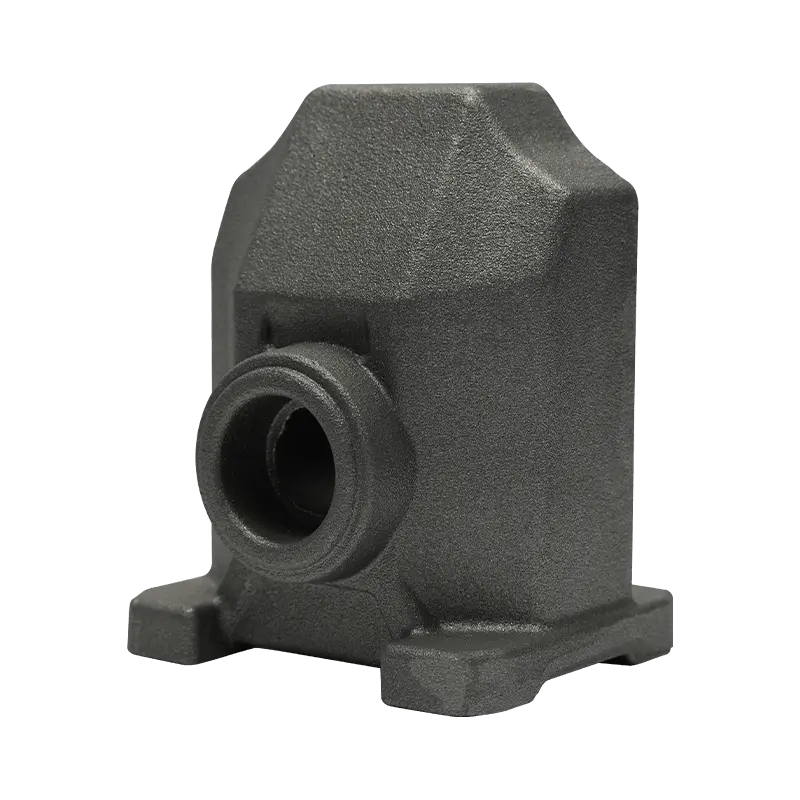
Grey Cast Iron Industrial Robot Accessories Foundry
Grey Cast Iron Industrial Robot Accessories specifically refers to industrial robot accessories made of high-quality grey cast iron. Grey cast iron is widely used in the field of industrial robots due to its good casting performance, good mechanical strength, wear resistance and vibration resistance. These accessories are precision-machined to improve the stability, durability and accuracy of the robot to meet the high-precision operation requirements in various complex industrial environments. From the robot arm connector, base support frame to the end effector mounting plate, each product strictly follows industry standards to ensure good compatibility with various industrial robot systems, helping to ensure efficient and stable operation of automated production lines.
ABOUT US
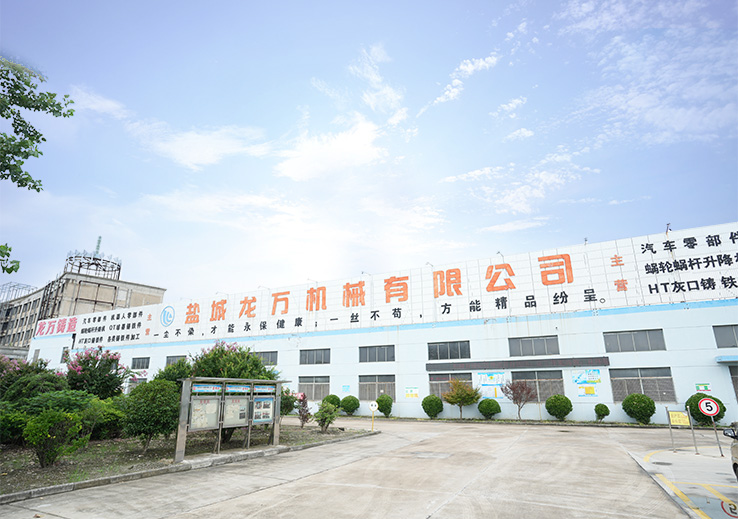
Yancheng Longwan Machinery Co., Ltd.
Founded in 2006, which located next to National Highway 204 in Yancheng City, Jiangsu Province, 40km from the center of Yancheng City, 5km from the center of Dongtai City, 30km from Dafeng District, and 10km from the exit of Baiju Expressway, with convenient transportation.
We mainly produce various types of fire-fighting pipe fittings, reducer parts, auto parts, agricultural machinery, and industrial robot parts. Its main customers include SAIC Group, Deere, Bonfiglioli (China), Shanghai Beixu, Yaskawa Electric, etc.
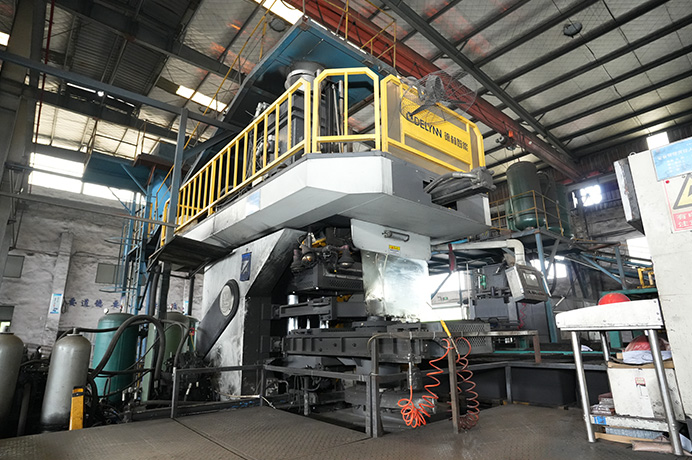
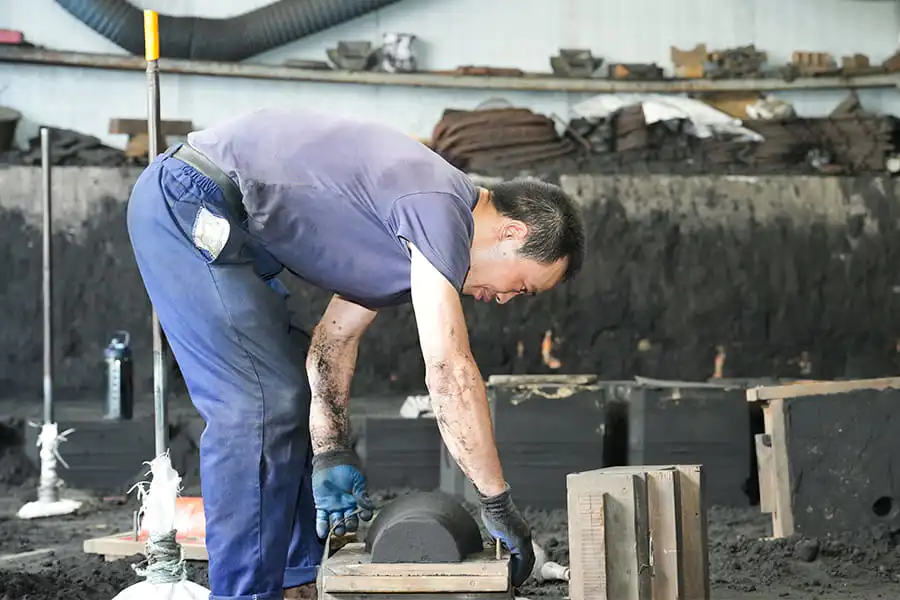
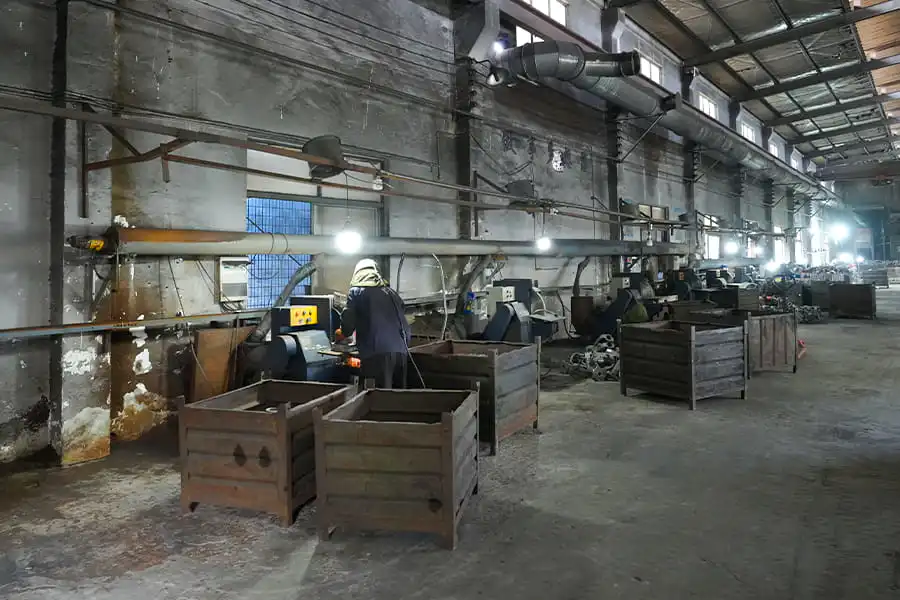
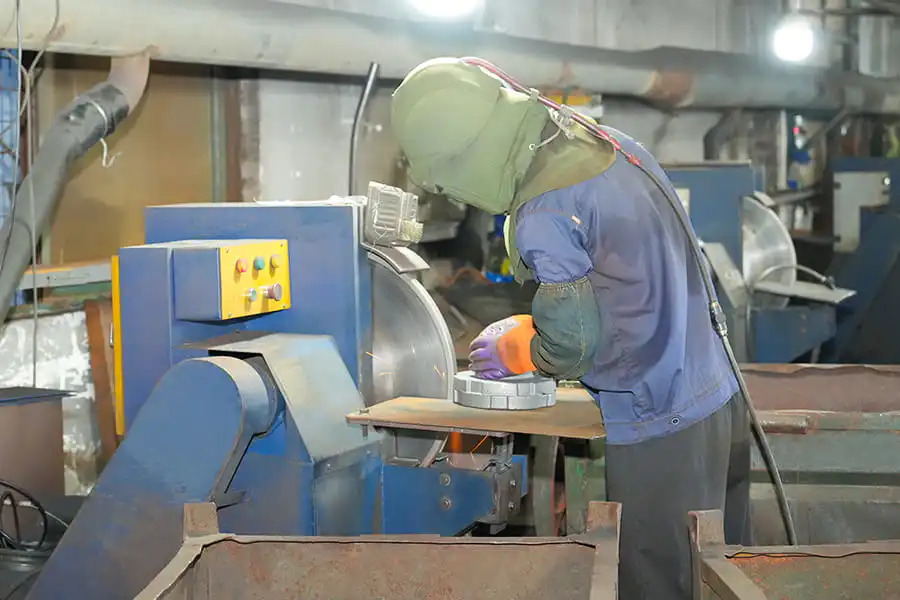
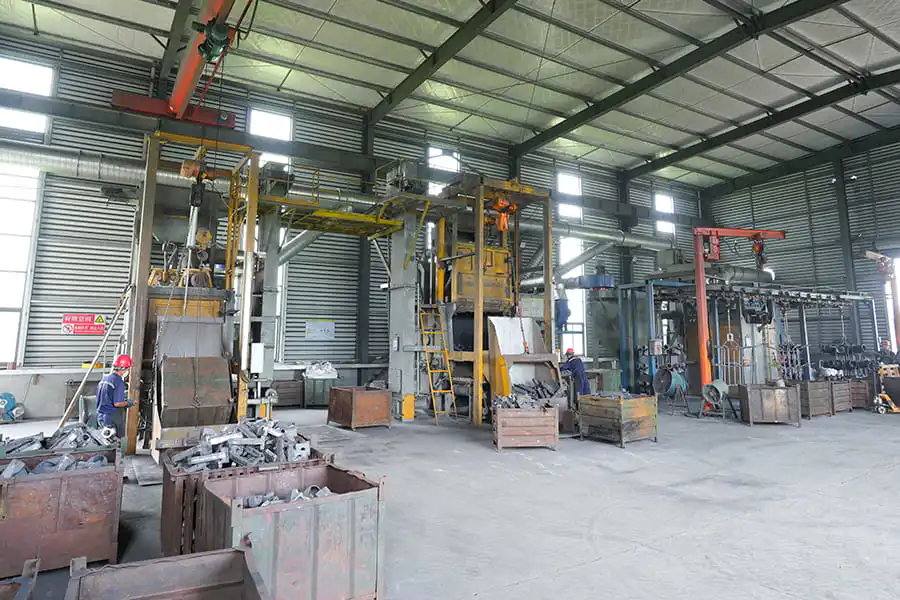
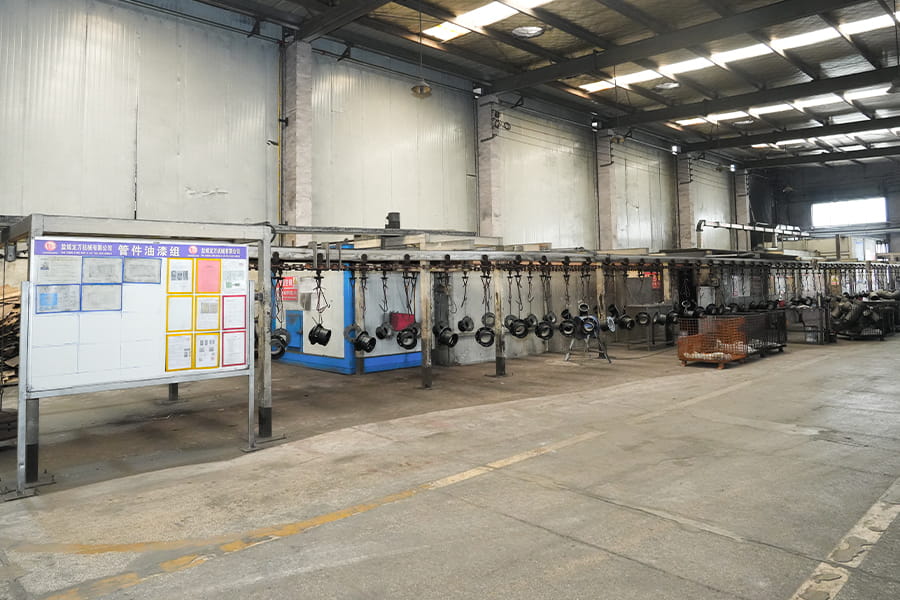
As a famous China Grey Cast Iron Industrial Robot Accessories Foundry and Grey Cast Iron Industrial Robot Accessories Suppliers, our company has a variety of molding equipment, including one vertical sand-shot horizontal parting boxless shot-press molding line with specifications of 610*510*240, 120 boxes/hour, suitable for mass production of small parts; one upper and lower sand-shot horizontal parting boxless shot-press molding line with specifications of 750*650*250, 100 boxes/hour, suitable for mass production of small and medium-sized parts; 3 sets of 1.25T medium-frequency electric furnaces; 3 cleaning shot blasting machines, and now planning a lost foam production line, suitable for 100Kg~1000Kg casting production, and planning an automatic spray painting line and an electrophoretic coating line at the same time, 3 CNC lathes and 3 lathes.
ODM Customization Expert
Advanced Production & Processing Equipment
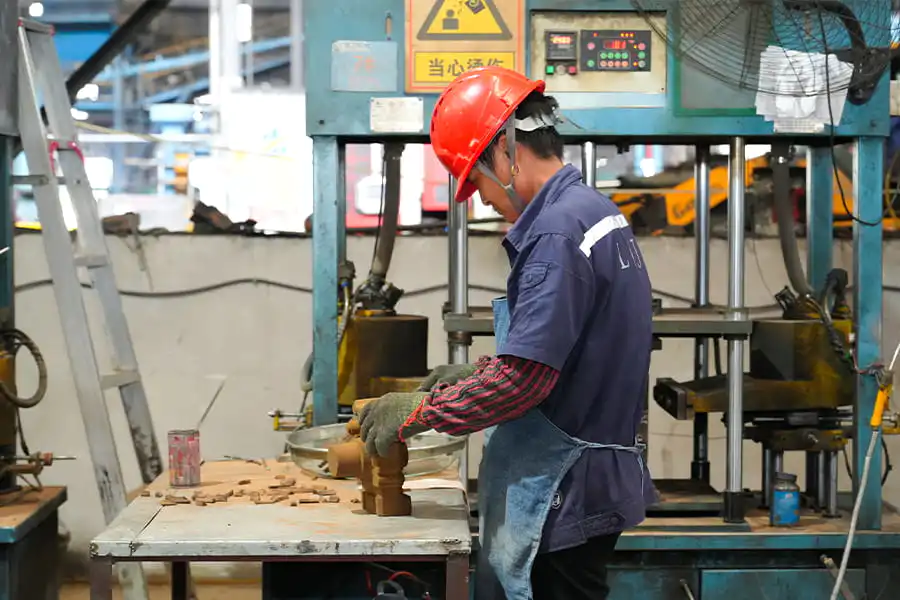
Longwan Machinery has a variety of advanced domestic and foreign molding equipment, including 2 fully automatic production lines for clay sand, 1 semi-automatic production line for clay sand, and 1 coated sand production line, with an annual production capacity of 15,000 tons.
Complete Inspection Flow
Strict Quality Inspection
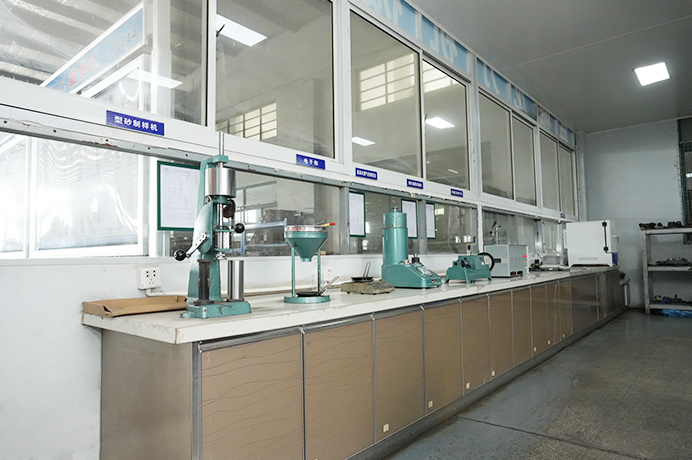
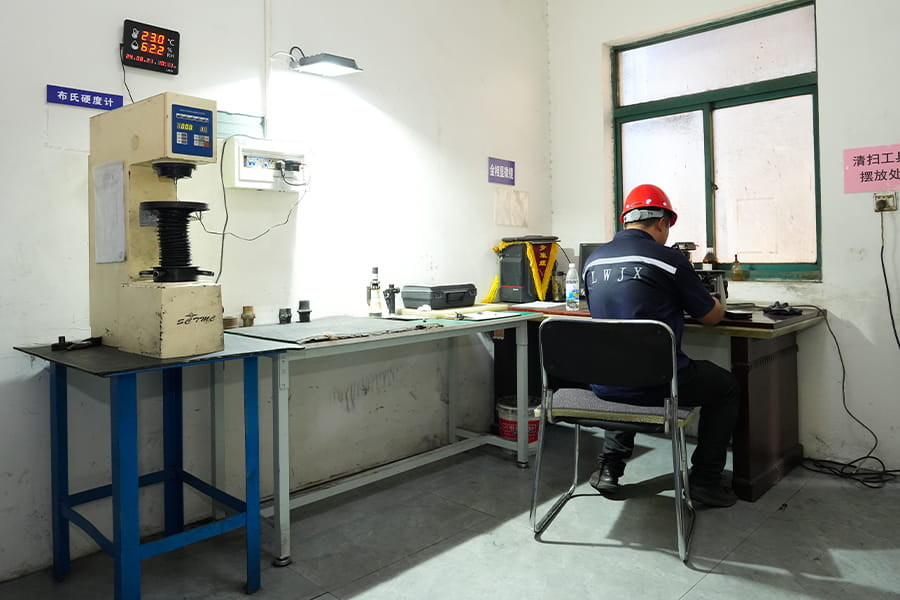
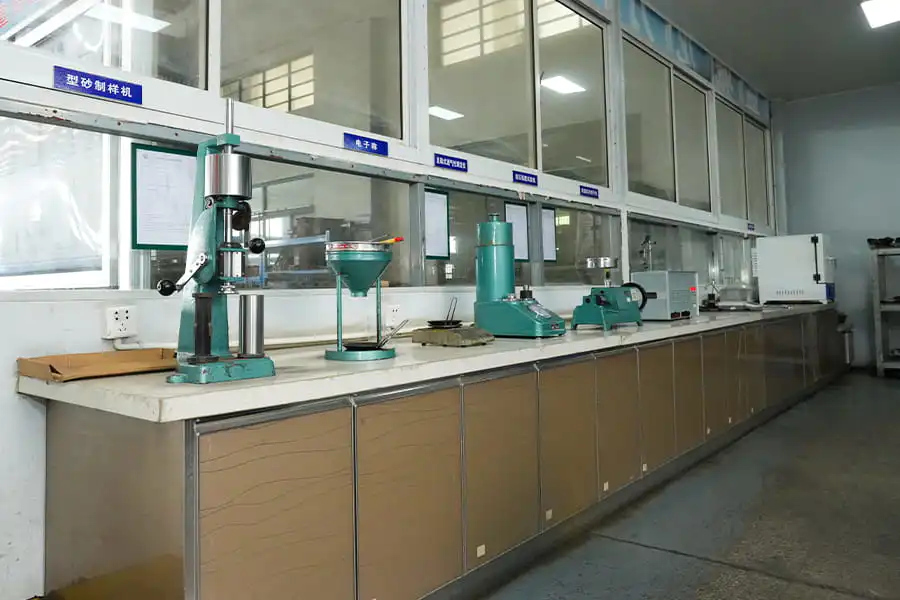
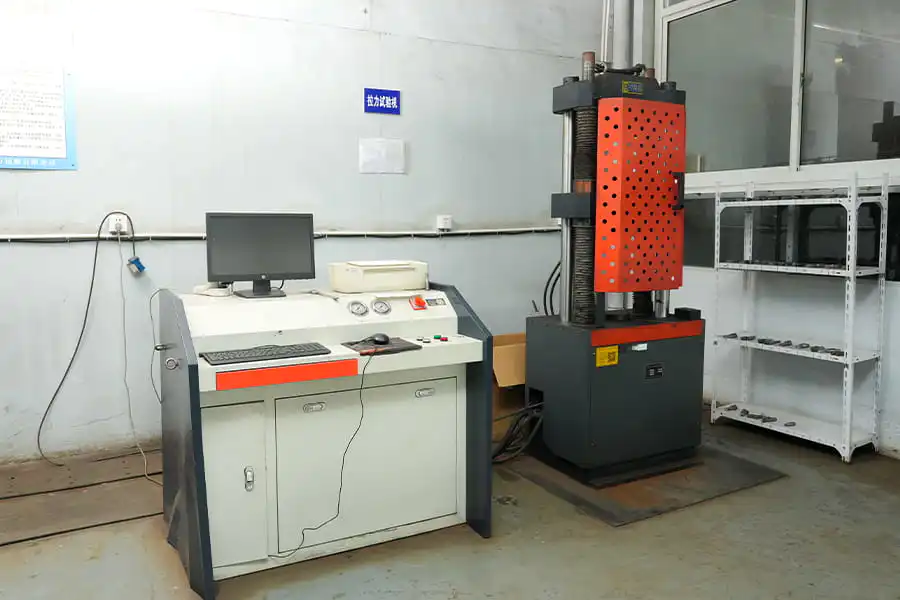
We have full-process testing equipment: spectrum analyzer, metallographic microscope, universal tensile testing machine, magnetic particle flaw detector, ultrasonic flaw detector, etc.
The above equipment can fully ensure that we can provide customers with high-precision final castings, and at the same time ensure that we meet customers' comprehensive testing requirements for physical and chemical properties of materials, non-destructive testing, high-precision geometric dimension testing, etc.
Professional Casting Expert
Comprehensive Casting Manufacturer
FAQ
-
QWhere are your products mainly exported to?A
Our products are mainly exported to multiple countries such as Germany, Japan, Italy, South Korea, and Australia.
-
QHow to deliver the goods to us?A
Usually, we ship by sea, which is very convenient for export.
Of course, if the customer's goods are urgent, we can also air freight them. Ningbo Airport and Shanghai International Airport are both very close to us.
-
QWhat's the payment term?A
When quoting, we will confirm the transaction method with you.
For mass production, we usually make a 50% advance payment in advance and then inspect and confirm the shipment before paying the remaining balance.
-
QHow to guarantee the quality of your goods?A
Firstly, there will be corresponding inspections after each process, and for the final completed product, we will conduct a full inspection according to customer requirements and international standards;
Then, we have advanced and complete top testing equipment in the industry: spectral analyzers, metallographic microscopes, universal tensile testing machines, magnetic particle testing machines, ultrasonic testing machines, etc.
The above equipment can fully ensure the provision of high-precision final castings to customers, while also meeting the comprehensive testing requirements of customers for material physical and chemical properties, non-destructive testing, high-precision geometric dimension testing, and so on.
-
QHow many employees of your company? what about the technicists?A
Our company has more than 120 employees, including 10 professional technicians and 5 engineers.
-
QHow about the capacity of your company?A
We have 2 fully automatic clay sand production lines, 1 semi-automatic clay sand production line, and 1 coated sand production line, with an annual production capacity of 15000 tons.
-
QDo you have some standard parts?A
No, currently we produce and customize according to the requirements based on the drawings provided by the customer.
-
QCan you do customized products?A
Yes, we are mainly doing customized products according to the customers’ drawings or samples.
-
QWhat applications do your products relate to?A
Our products cover almost all the applicable equipment manufacturing and machinery manufacturing and processing fields, mainly including automotive trucks, engineering machinery, agricultural machinery, reducers, water pumps, water treatment systems, and other fields.
-
Qwhat products can you offer?A
We mainly produce cast iron parts made of gray cast iron and ductile iron materials.
-
QAre you a direct manufacturer or trading company?A
We are a foundry and a manufacturer of cast iron parts.
-
QHow long can I get the feedbacks after we sent the inquiry?A
We will reply to you within 24 hours of the working day.
NEWS
-
How to Connect Ductile Iron Pipe: Joint Types, Assembly Steps, and Best Practices
Ductile iron pipe has earned a well-deserved place in water distribution, fire protection, and drainage systems. It is strong, impact-resistant, and ...
READ MORE -
How Is Grey Cast Iron Made? A Foundry's Step-by-Step Guide to Sand Casting
Grey cast iron has been poured into sand moulds for centuries, yet the questions buyers ask have barely changed: what actually goes into the furnace,...
READ MORE -
How Many Types of Cast Iron Are There? Four Main Types and Two Extended Families
Ask a room full of foundry engineers how many types of cast iron are there, and you will usually hear two numbers: four, or six. Both answers are cor...
READ MORE -
How Does Carbon Affect Steel? Understanding Strength, Hardness & Ductility
Carbon is the single most influential alloying element in steel. A shift of just a few tenths of a percent can turn a soft, bendable sheet into a har...
READ MORE
Grey Cast Iron Industrial Robot Accessories Industry knowledge
Yancheng Longwan Machinery Co., Ltd. is a Jiangsu foundry producing grey and ductile iron castings to customer drawings. Industrial robot parts are one of our established product families, alongside automotive, agricultural machinery, reducer and fire-fighting fitting castings. We supply grey cast iron arm connectors, base support frames and end effector mounting plates as rough, semi-finished or machined castings, working directly from a drawing or a physical sample.
The range is built around rigid, damped structures: castings that hold geometry through repeated motion cycles, absorb vibration before it reaches the tool or workpiece, and accept machined locating features without distortion. We operate as a Grey Cast Iron Industrial Robot Accessories manufacturer, casting to the grade, machining scope and inspection plan agreed for each robot programme.
Our Grey Cast Iron Industrial Robot Accessories Range
The parts we cast for robot builders and integrators fall into a small number of repeating structural functions. Each is quoted as a custom casting, because the interface geometry is specific to your arm or cell design.
- Arm connectors and joint housings that join arm segments across bolted interfaces.
- Base support frames and mounting plates that anchor axis 1 to a pedestal, plinth or floor plate.
- End effector mounting plates and tool flanges carrying the tool interface and payload.
- Bearing housings and shaft supports locating wrist or counterbalance shafts.
- Counterweights and ballast blocks for torque offset and motion stability.
- Dress-pack brackets and cable guides routing harness and hoses along the arm.
Where Each Robot Accessory Type Fits
| Component family | Function in the robot | Design drivers | What we confirm |
|---|---|---|---|
| Arm connector / joint housing | Joins arm segments; carries bending and torsional load | Wall thickness, bolt circle, rib layout, bore alignment, draft | Grade and hardness, machining allowance, datum faces |
| Base support frame / mounting plate | Anchors the first axis to floor or pedestal | Footprint stiffness, anchor pattern, flatness, mass for stability | Mould box selection, machine datum, cast weight |
| End effector mounting plate / tool flange | Carries tool interface and payload | Thickness, hole pattern position, face flatness, edge stiffness | Machining scope, fit tolerance, part marking |
| Bearing housing / shaft support | Locates wrist or counterbalance shafts | Bore tolerance, concentricity, uniform wall section | Core design, gating, bore inspection method |
| Counterweight / ballast block | Offsets arm torque and damps motion | Mass tolerance, density consistency, lifting points | Cast weight control, pouring practice, surface finish |
| Dress-pack bracket / cable guide | Routes harness, hoses and sensors along the arm | Minimum section, corner radii, vibration resistance | Minimum section for filling, edge quality, finish |
Why Grey Cast Iron Suits Robot Structures
Grey cast iron carries graphite in flake form, which is the reason it is used on machine frames and robot bases rather than as a general substitute for steel or ductile iron.
- Vibration damping. The flake graphite structure absorbs energy, which reduces resonance in arm segments and base plates.
- Wear resistance. Suitable for sliding and locating surfaces where abrasion resistance matters.
- Castability. Ribs, pockets and thick-to-thin transitions are produced in one pour, which is difficult to achieve economically in fabricated assemblies.
- Thermal and dimensional stability. Section stiffness is retained across the working temperature range of a normal production cell.
- Machinability. Turned bores, faces and grooves are produced cleanly, with good surface finish at the mating interface.
Production Route, Capacity and Equipment
Robot accessories run on our clay sand and coated sand lines, with the shot-press moulding lines assigned according to part size and order volume.
| Stage | Equipment | What it delivers |
|---|---|---|
| Pattern and mould making | 2 fully automatic clay sand lines, 1 semi-automatic clay sand line, 1 coated sand line; vertical shot-press boxless line 610 x 510 x 240 mm at 120 boxes/hour; upper/lower shot-press line 750 x 650 x 250 mm at 100 boxes/hour | Repeatable moulds for small and small-to-medium robot castings in volume |
| Melting and pouring | 3 x 1.25 T medium-frequency electric furnaces | Controlled chemistry and pouring temperature for grey iron grades |
| Cleaning and finishing | 3 shot blasting machines; grinding and polishing lines | Sand-free surface ready for machining or coating |
| Machining | 3 CNC lathes and 3 lathes | Turned diameters, faces, bores and grooves at mating interfaces |
| Coating (planned) | Automatic spray painting line and electrophoretic coating line | Corrosion protection as an in-house finishing step |
| Programme capacity | Lines above, 15,000 t annual output | Support for repeat orders and multi-year robot programmes |
Configuration and Machining Options
Robot accessories are quoted in the delivery state that matches your assembly sequence. We agree the cast-to and machined-to boundaries before patterns are cut, so that locating faces, bores and bolt patterns are generated from the same datum.
- Delivery state: as-blasted rough casting, semi-finished with machining allowance, or finish-machined turned features.
- Material: grey iron cast to the grade and hardness range on your drawing, with test bars poured from the same batch.
- Geometry: rib layout, pocket depth, boss height and section transitions reviewed against moulding practice and draft.
- Interfaces: spigot diameters, flange thickness and bore sizes held to the tolerances you set on the drawing.
- Finishing: surface preparation and paint or electrophoretic coating where the specification calls for it.
- Identification: part marking and traceability applied as agreed, including batch reference for material records.
Quality Control and Acceptance Testing
Our foundry works to a complete IATF 16949:2016 system standard, with inspection at each process step and a final inspection of finished parts against the drawing and the agreed standard. Robot accessory programmes typically combine material verification, non-destructive checks and dimensional inspection.
- German SPECTRO direct-reading spectrometer for chemical composition.
- Universal tensile testing machine and 3T Brinell hardness tester for mechanical properties.
- Metallographic microscope and sonic velocity meter for structure and consistency checks.
- Magnetic particle and ultrasonic flaw detection where the specification requires it.
- Moulding sand testing with SAC hammer-type sample making machine, SWY hydraulic strength testing machine, SSZ vibration-type sand screening machine and SGS double-disc infrared dryer.
Project Flow from Drawing to Shipment
- Drawing confirmation and quotation against the agreed delivery state.
- Pattern and mould manufacture after the mould order is released.
- Sample castings produced from the mould and submitted for your approval.
- Mass production after sample confirmation and order release.
- Inspection by our inspectors, or jointly with your team, on completion.
- Packing and shipment once inspection results and release are confirmed.
Information We Use to Configure Your Solution
| Input | Detail we work from | How it shapes the proposal |
|---|---|---|
| Drawing or 3D model | Latest revision with all views and section notes | Pattern design, mould box selection, machining allowance |
| Material specification | Grade, tensile class, hardness range | Charge mix, melting practice, test plan |
| Machining scope | Faces, bores, diameters, tolerances and datums | Semi-finished or finished delivery state |
| Interface data | Bolt pattern, spigot diameters, flange thickness | Datum choice and dimensional inspection plan |
| Volume and call-off | Annual quantity, batch size, delivery rhythm | Mould type and production line assignment |
| Finishing and documentation | Coating, part marking, traceability, inspection records | Finishing route, packing method, shipment release |
Packing, Delivery and Support
Castings are packed for sea freight as standard, with air freight used when a programme is time-critical; Ningbo and Shanghai airports are both within easy reach of the foundry. Packing design can be adapted to your handling and storage requirements, and technical enquiries are answered within 24 hours of the working day.
Robot castings from our works already run in programmes for customers including Yaskawa Electric, SAIC Group, Deere and Bonfiglioli (China). Parts are exported to Germany, Japan, Italy, South Korea and Australia, and we quote against drawings or samples with no catalogue standard parts.
Related Cast Iron Ranges
Where an application calls for higher impact resistance than flake graphite iron can give, we cast the equivalent parts in Ductile Cast Iron Industrial Robot Accessories. The wider catalogue is organised under Grey Cast Iron, and the whole cast iron casting range is produced in the same Yancheng foundry.
Frequently Asked Questions
Which grey iron grades do you cast for robot accessories?
We cast to the grade and hardness stated on your drawing. For load-bearing robot structures that is normally a pearlitic grey iron, and composition is verified on the German SPECTRO spectrometer, hardness on the 3T Brinell tester and tensile properties on the universal testing machine from the same pour.
What part sizes can you produce in this family?
Our shot-press moulding boxes are 610 x 510 x 240 mm and 750 x 650 x 250 mm, capable of 120 and 100 boxes per hour respectively, which suits volume production of small and small-to-medium robot castings. A lost foam line is planned to extend coverage into the 100 kg to 1000 kg casting range.
Do you hold standard robot accessory parts in stock?
No. We manufacture to the drawing or sample you provide, in OEM and ODM mode, which is why base frames, tool plates and joint housings are quoted individually rather than selected from a shelf list.
How is quality verified before shipment?
Inspection runs after each process step, and finished castings receive a final inspection against the drawing. Depending on the specification we apply spectrometry, metallography, tensile and Brinell testing, magnetic particle or ultrasonic flaw detection, and dimensional checks on the machined interfaces.
Can you machine and coat the castings in-house?
Turned features such as bores, faces, diameters and grooves are produced on our 3 CNC lathes and 3 lathes. Shot blasting and grinding prepare the surface, and an automatic spray painting line and electrophoretic coating line are planned as in-house finishing steps.
Longwan Machinery adheres to the corporate purpose of "High
quality, good reputation, customer priority, service precedence".
- Service
- ODM & OEM
- CAPACITIES
- Contact Infor.
- [email protected]
- +86-515-83658999
- +86-152 5109 2111
- Group 2, Dingxi Village, Caoyan Town, Dafeng District, Yancheng City, Jiangsu, China
Mobile QR Code
Copyright © 2024 Yancheng Longwan Machinery Co., Ltd.All Rights Reserved.
Powder By: 
OEM/ODM Grey Cast Iron Industrial Robot Accessories Foundry
