


 English
 русский
 Deutsch

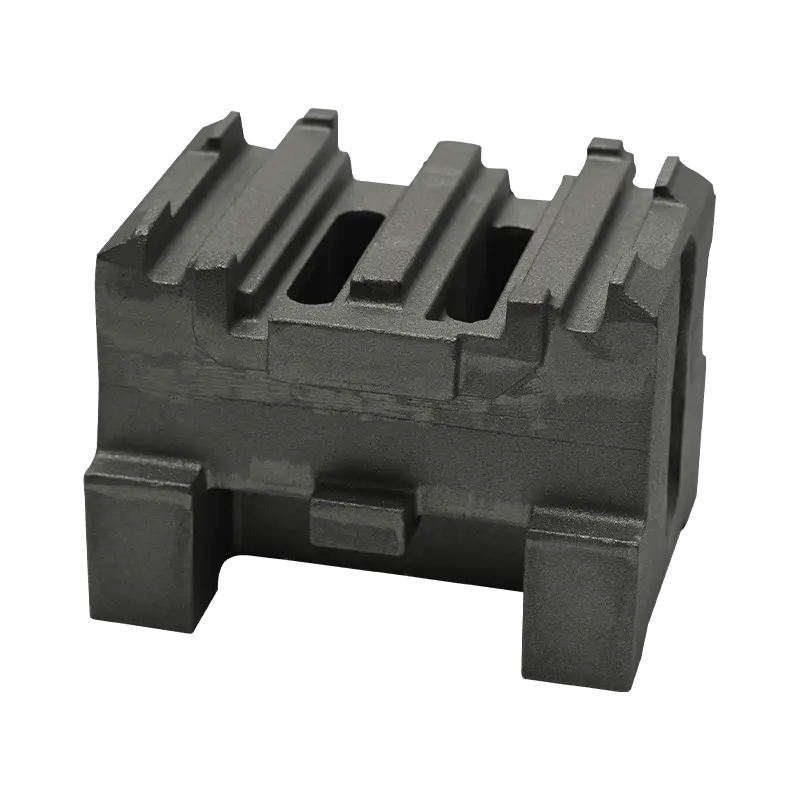
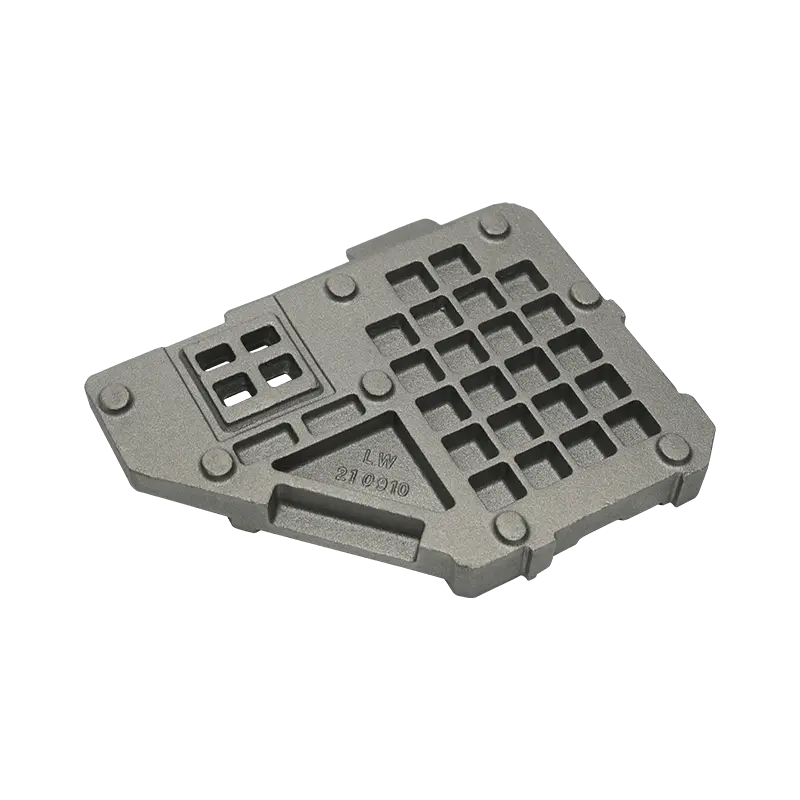
Ductile Cast Iron Semiconductor Accessories Foundry
Ductile Cast Iron is used in the semiconductor industry as a base and other accessories, demonstrating its good mechanical properties and stability. As a key component for supporting and fixing semiconductor equipment, the base needs to have high strength, heat resistance and corrosion resistance to ensure the stability and reliability of the equipment. Ductile Cast Iron can effectively disperse and transfer the heat generated by the equipment through its uniform structure and good thermal conductivity, thereby extending the service life of the equipment and improving its performance.
ABOUT US
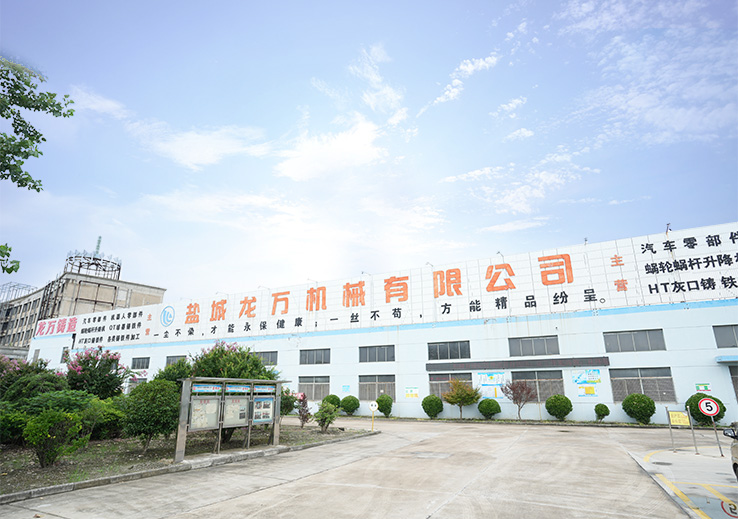
Yancheng Longwan Machinery Co., Ltd.
Founded in 2006, which located next to National Highway 204 in Yancheng City, Jiangsu Province, 40km from the center of Yancheng City, 5km from the center of Dongtai City, 30km from Dafeng District, and 10km from the exit of Baiju Expressway, with convenient transportation.
We mainly produce various types of fire-fighting pipe fittings, reducer parts, auto parts, agricultural machinery, and industrial robot parts. Its main customers include SAIC Group, Deere, Bonfiglioli (China), Shanghai Beixu, Yaskawa Electric, etc.
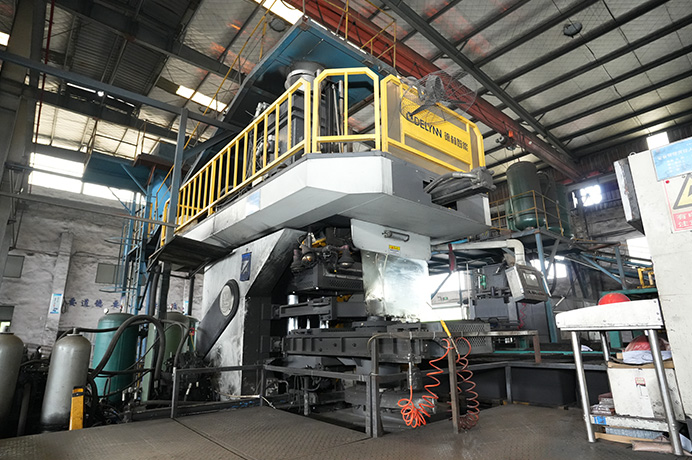
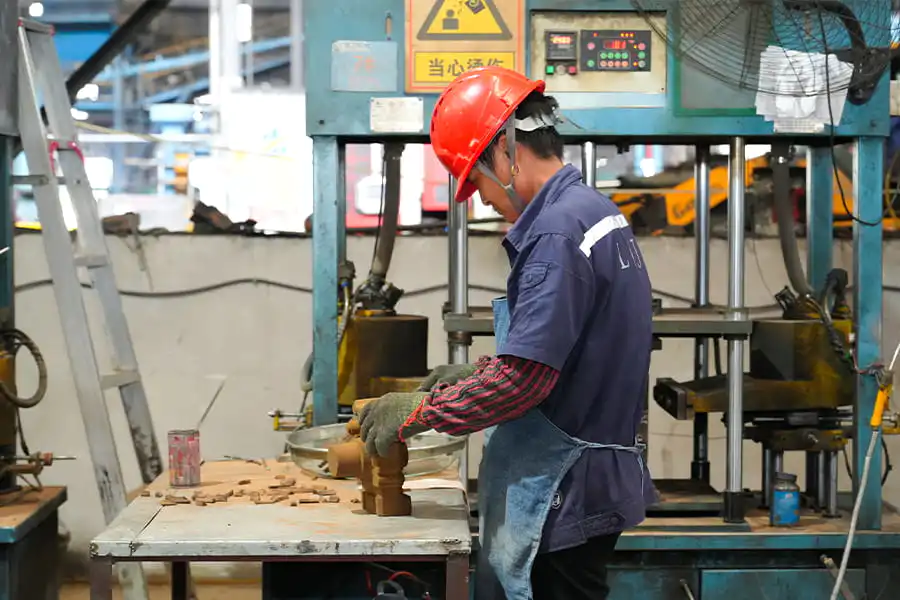
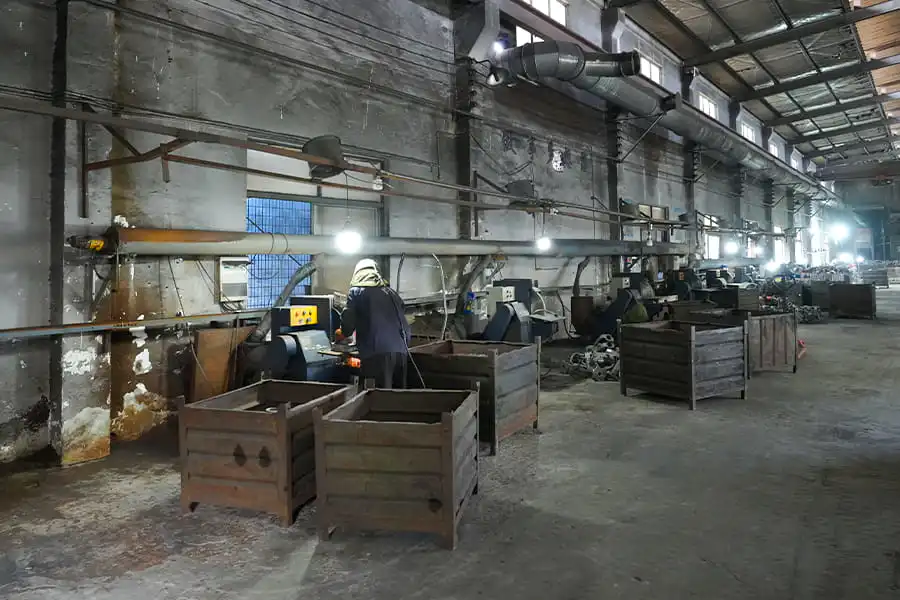
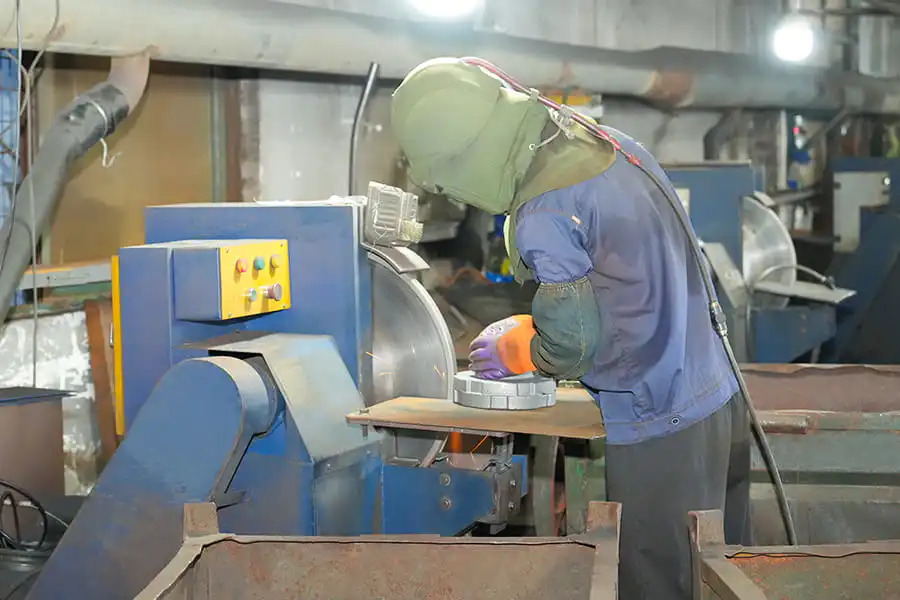
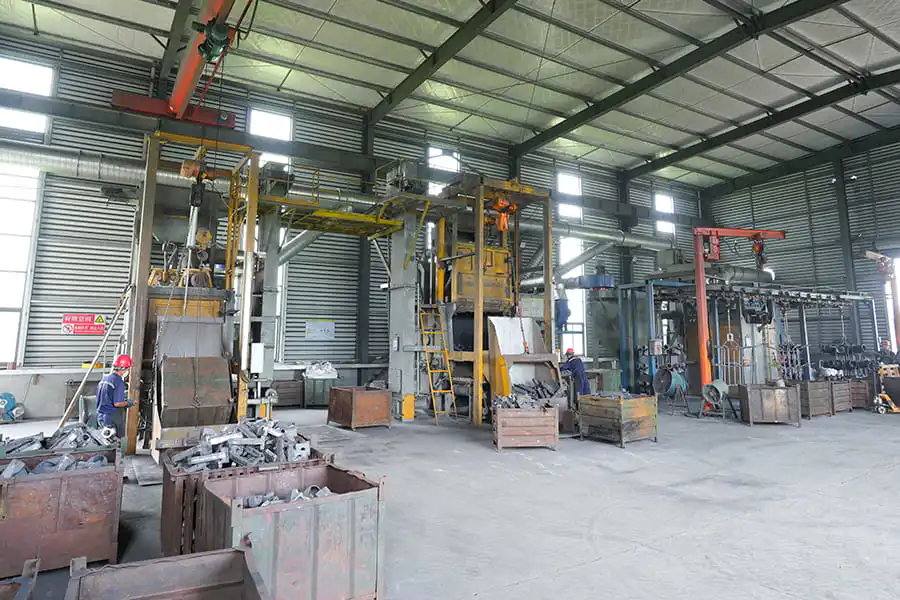
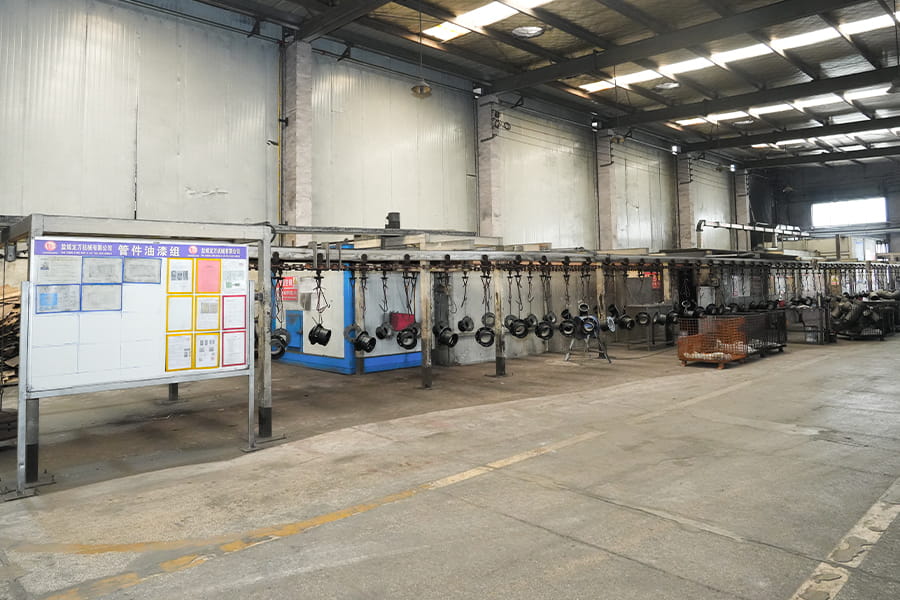
As a famous China Ductile Cast Iron Semiconductor Accessories Foundry and Ductile Cast Iron Semiconductor Accessories Suppliers, our company has a variety of molding equipment, including one vertical sand-shot horizontal parting boxless shot-press molding line with specifications of 610*510*240, 120 boxes/hour, suitable for mass production of small parts; one upper and lower sand-shot horizontal parting boxless shot-press molding line with specifications of 750*650*250, 100 boxes/hour, suitable for mass production of small and medium-sized parts; 3 sets of 1.25T medium-frequency electric furnaces; 3 cleaning shot blasting machines, and now planning a lost foam production line, suitable for 100Kg~1000Kg casting production, and planning an automatic spray painting line and an electrophoretic coating line at the same time, 3 CNC lathes and 3 lathes.
ODM Customization Expert
Advanced Production & Processing Equipment
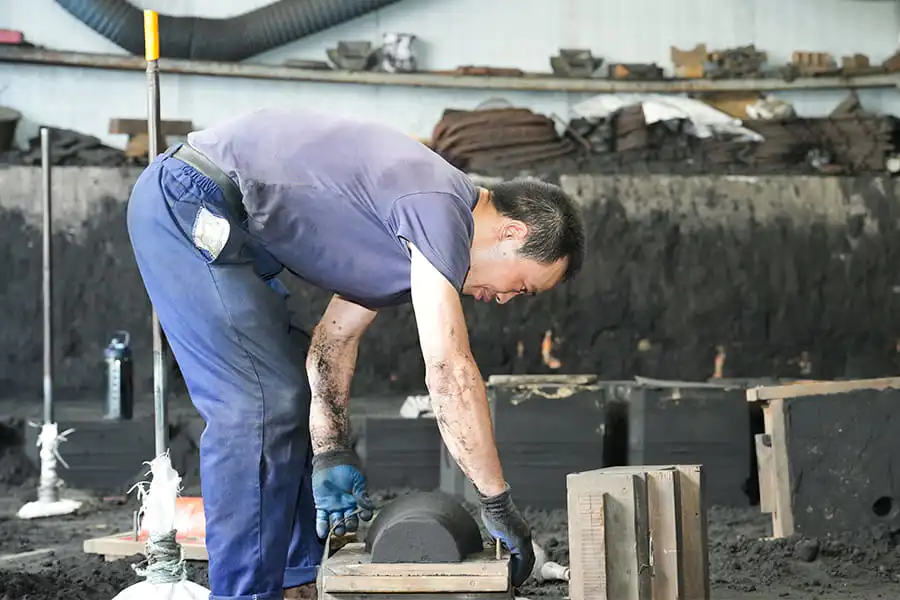
Longwan Machinery has a variety of advanced domestic and foreign molding equipment, including 2 fully automatic production lines for clay sand, 1 semi-automatic production line for clay sand, and 1 coated sand production line, with an annual production capacity of 15,000 tons.
Complete Inspection Flow
Strict Quality Inspection
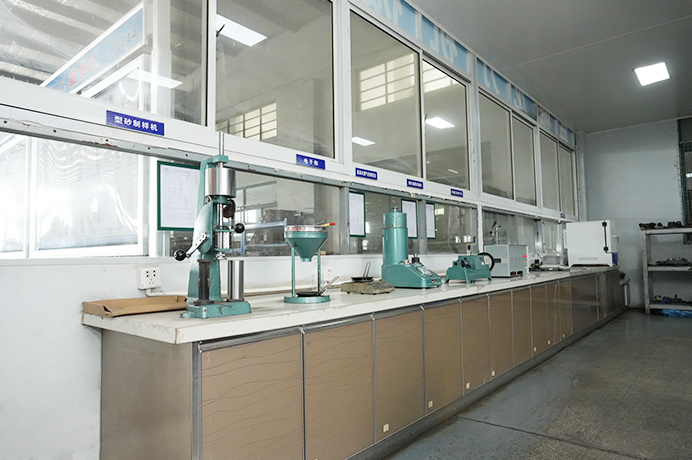
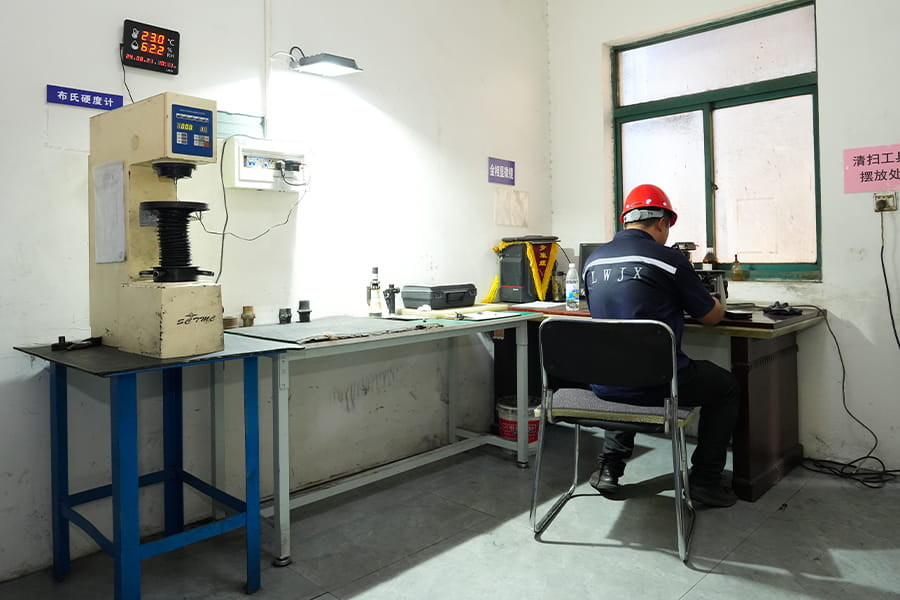
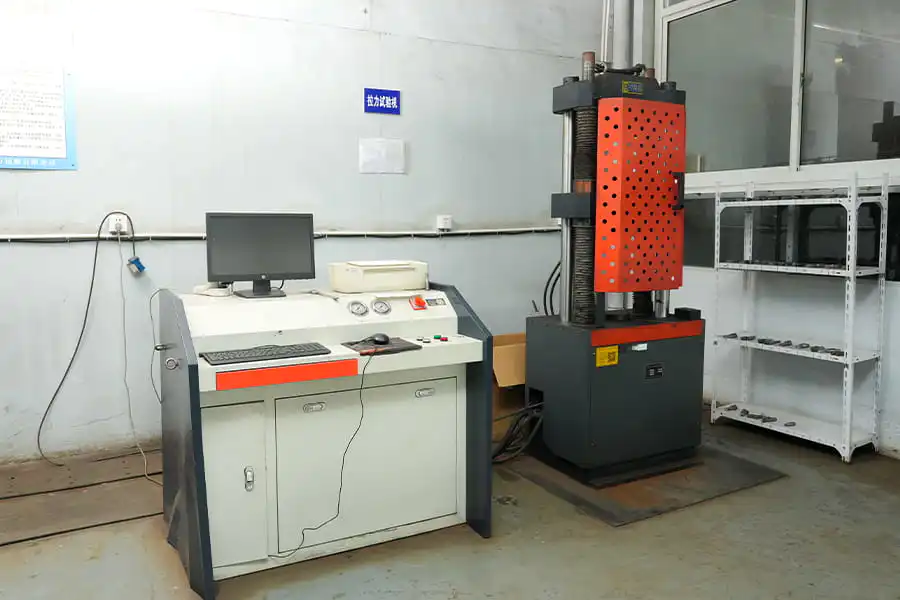
We have full-process testing equipment: spectrum analyzer, metallographic microscope, universal tensile testing machine, magnetic particle flaw detector, ultrasonic flaw detector, etc.
The above equipment can fully ensure that we can provide customers with high-precision final castings, and at the same time ensure that we meet customers' comprehensive testing requirements for physical and chemical properties of materials, non-destructive testing, high-precision geometric dimension testing, etc.
Professional Casting Expert
Comprehensive Casting Manufacturer
FAQ
-
QWhere are your products mainly exported to?A
Our products are mainly exported to multiple countries such as Germany, Japan, Italy, South Korea, and Australia.
-
QHow to deliver the goods to us?A
Usually, we ship by sea, which is very convenient for export.
Of course, if the customer's goods are urgent, we can also air freight them. Ningbo Airport and Shanghai International Airport are both very close to us.
-
QWhat's the payment term?A
When quoting, we will confirm the transaction method with you.
For mass production, we usually make a 50% advance payment in advance and then inspect and confirm the shipment before paying the remaining balance.
-
QHow to guarantee the quality of your goods?A
Firstly, there will be corresponding inspections after each process, and for the final completed product, we will conduct a full inspection according to customer requirements and international standards;
Then, we have advanced and complete top testing equipment in the industry: spectral analyzers, metallographic microscopes, universal tensile testing machines, magnetic particle testing machines, ultrasonic testing machines, etc.
The above equipment can fully ensure the provision of high-precision final castings to customers, while also meeting the comprehensive testing requirements of customers for material physical and chemical properties, non-destructive testing, high-precision geometric dimension testing, and so on.
-
QHow many employees of your company? what about the technicists?A
Our company has more than 120 employees, including 10 professional technicians and 5 engineers.
-
QHow about the capacity of your company?A
We have 2 fully automatic clay sand production lines, 1 semi-automatic clay sand production line, and 1 coated sand production line, with an annual production capacity of 15000 tons.
-
QDo you have some standard parts?A
No, currently we produce and customize according to the requirements based on the drawings provided by the customer.
-
QCan you do customized products?A
Yes, we are mainly doing customized products according to the customers’ drawings or samples.
-
QWhat applications do your products relate to?A
Our products cover almost all the applicable equipment manufacturing and machinery manufacturing and processing fields, mainly including automotive trucks, engineering machinery, agricultural machinery, reducers, water pumps, water treatment systems, and other fields.
-
Qwhat products can you offer?A
We mainly produce cast iron parts made of gray cast iron and ductile iron materials.
-
QAre you a direct manufacturer or trading company?A
We are a foundry and a manufacturer of cast iron parts.
-
QHow long can I get the feedbacks after we sent the inquiry?A
We will reply to you within 24 hours of the working day.
NEWS
-
How Is Grey Cast Iron Made? A Foundry's Step-by-Step Guide to Sand Casting
Grey cast iron has been poured into sand moulds for centuries, yet the questions buyers ask have barely changed: what actually goes into the furnace,...
READ MORE -
How Many Types of Cast Iron Are There? Four Main Types and Two Extended Families
Ask a room full of foundry engineers how many types of cast iron are there, and you will usually hear two numbers: four, or six. Both answers are cor...
READ MORE -
How Does Carbon Affect Steel? Understanding Strength, Hardness & Ductility
Carbon is the single most influential alloying element in steel. A shift of just a few tenths of a percent can turn a soft, bendable sheet into a har...
READ MORE -
How Is Ductile Iron Pipe Made? Inside the Foundry Process Step by Step
Ductile iron pipe has served as a backbone of modern water systems for decades. Engineers choose it because it combines pressure capacity, impact res...
READ MORE
Ductile Cast Iron Semiconductor Accessories Industry knowledge
Ductile Cast Iron Semiconductor Accessories Cast to Your Equipment Drawing
Yancheng Longwan Machinery Co., Ltd. is a ductile iron and grey iron foundry in Yancheng City, Jiangsu Province, casting and finishing load-bearing accessories for semiconductor equipment: stage and machine bases, frame plates, housing bodies, load-port brackets, fixture pads and cooling manifold bodies. We work from customer drawings or physical samples under an OEM/ODM model, so the base that carries a wafer stage or the housing that locates a vacuum pump is quoted against its own material grade, wall section, machining allowance and inspection plan rather than a fixed catalogue number.
As a China Ductile Cast Iron Semiconductor Accessories manufacturer, we handle pattern making, melting, molding, shot blasting, turning and coating preparation as one project, with process testing at every stage before the casting reaches your assembly floor.
Our Semiconductor Accessory Range and Where Each Part Fits
Semiconductor tooling is a vibration-sensitive, temperature-cycling environment. Ductile iron suits these parts because its nodular graphite structure combines tensile strength, damping and thermal stability in a casting that can still be produced in thick, ribbed geometries. Our range covers:
- Equipment bases and bed plates — support structures for stages, metrology stations and inspection platforms.
- Frame and gantry components — carrying linear motion rails, gantry beams and structural tie plates.
- Housing and chamber supports — bodies and feet that locate vacuum chambers, pumps and gas panels.
- Load-port and handling brackets — reference parts for wafer transfer arms and carrier interfaces.
- Fixture and tooling pads — clamping plates, mask holders and carrier reference faces.
- Cooling and manifold bodies — coolant distribution blocks with machined port faces.
| Part group | Function in the tool | Specification focus | Configuration notes |
|---|---|---|---|
| Machine and stage bases | Support wafer stage, metrology or inspection platform | Section thickness, rib layout, machined face flatness, damping behaviour | As-cast or fully machined; leveling bosses cast in |
| Frame and gantry plates | Carry linear rails and gantry structures | Flatness, hole pattern position, wall stiffness | Datum scheme and per-face machining allowance confirmed |
| Housing and chamber supports | Locate chambers, pumps and gas panels | Wall soundness, tightness where specified, mounting faces | Ultrasonic or magnetic particle testing when drawn |
| Load-port and handling brackets | Position wafer transfer and handling arms | Hole-to-hole accuracy, thread depth, vibration behaviour | Machined pads and dowel bores preferred over cast threads |
| Fixture and tooling pads | Clamp wafers, carriers and masks | Surface finish, parallelism, edge break | Coating selected where wipe-down cleaning is used |
| Cooling and manifold bodies | Distribute coolant from chillers to tool modules | Core soundness, internal cleanliness, port face flatness | Machined port faces and internal cleaning to drawing note |
Material Grade Selection for Semiconductor Duty
Grade is taken from the customer drawing or agreed during the sample stage. Nodular iron grades used for bases, frames and housings typically run from about 400 MPa to 700 MPa minimum tensile strength, with elongation from roughly 2% to 18% depending on whether a ferritic or pearlitic matrix is required. Wall thickness, rib spacing and machining allowance follow from the load path and the mounting interface, not from a single house standard.
- Thermal behaviour — uniform graphite distribution spreads heat from drive and process zones, and the low coefficient of thermal expansion relative to aluminium keeps reference faces stable through warm-up cycles.
- Vibration damping — graphite nodules absorb energy that would otherwise reach wafer alignment optics and positioning stages.
- Surface protection — since iron is not inherently corrosion resistant, painted and coated finishes are specified for parts exposed to cleaning agents and humid service air.
- Comparable cast irons — where damping matters more than elongation, Grey Cast Iron Semiconductor Accessories are an alternative we cast on the same lines.
Configuration Options We Build Into the Casting
Each project is configured around the drawing set and the assembly sequence. Pattern and core design, gating, feeding and machining allowance are settled before the first sample is poured, and we record what changed between sample and production so the released process stays repeatable.
- Supply condition — as-cast, shot blasted, primed, painted or coated, quoted per part.
- Machining — turning on CNC lathes and lathes; bores, face turning and step features are quoted against the drawing tolerance.
- Inserts and hardware — threaded inserts, dowel bores and reference pads are defined by the equipment builder, not left to the foundry.
- Marking — part number, heat identification and traceability marking to the drawing or your packaging specification.
- Coating lines — an automatic paint line and an electrophoretic coating line are in planning for parts that need consistent film thickness.
Foundry Capacity and Repeatability
Yancheng Longwan Machinery runs two fully automatic clay sand lines, one semi-automatic clay sand line and one coated sand line, with an annual production capacity of 15,000 tons. Molding equipment is matched to part size so small brackets and medium housings run on the line that gives the best box utilisation and cycle stability.
- Vertical sand-shot horizontal parting boxless line, 610 × 510 × 240 mm, 120 boxes per hour — high-volume small semiconductor fittings.
- Upper and lower sand-shot horizontal parting boxless line, 750 × 650 × 250 mm, 100 boxes per hour — small to medium bases and housings.
- Three 1.25T medium-frequency electric furnaces for consistent melt chemistry.
- Three cleaning shot blasting machines and three CNC lathes with three lathes.
- A lost foam line for 100 kg to 1000 kg castings is under development for heavier frame and base structures.
Quality Control and Acceptance Testing
Inspection is embedded in the route rather than applied only at the end. We operate under an IATF 16949:2016 system standard, with material performance and molding sand testing carried out in house and final parts verified against the agreed inspection plan before shipment.
- German SPECTRO direct-reading spectrometer for melt chemistry.
- Tensile testing machine, 3T Brinell hardness tester, sonic velocity meter and metallographic microscope for matrix and nodularity checks.
- Magnetic particle and ultrasonic flaw detection for soundness where the drawing requires it.
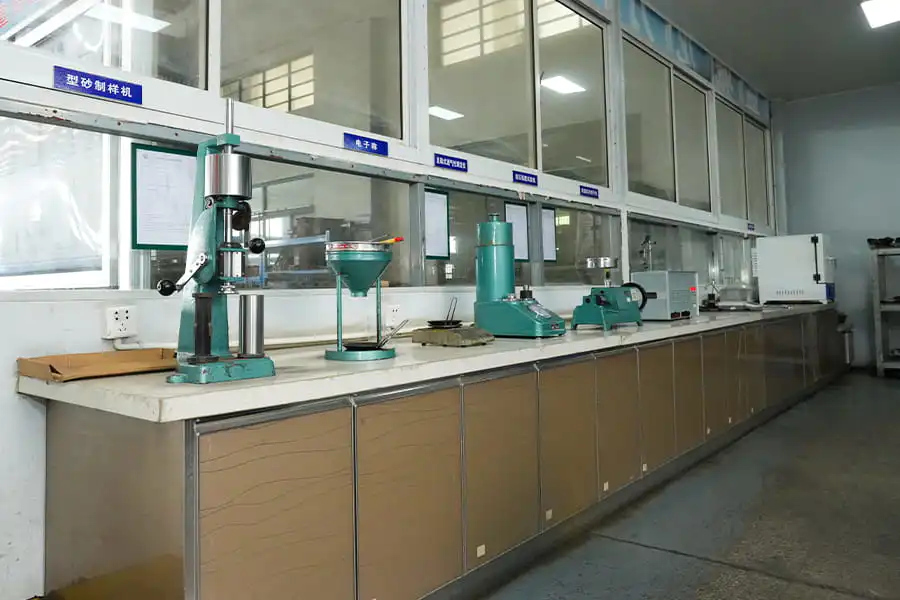
- SAC hammer-type sample making machine, SWY hydraulic strength testing machine, SSZ vibration sand screening machine and SGS double-disc infrared dryer for sand control.
- Dimensional reports, material certificates and NDT records issued to the acceptance scope agreed at order.
Installation, Serviceability and Project Support
Semiconductor accessories are installed into assemblies that are already aligned and levelled, so we review lifting points, leveling pad locations, jacking faces and access for fastening before the pattern is approved. Reference faces are identified on the drawing so turning and inspection use the same datums the tool builder uses at final assembly.
Maintenance planning is part of the same conversation. Where a fixture pad or handling bracket is a wear item, we keep pattern records, material grade and process route on file so repeat orders reproduce the released condition. This is also how we support neighbouring product families such as Ductile Cast Iron Industrial Robot Accessories and the wider Ductile Cast Iron programme on the same quality system.
Information We Use to Configure Your Solution
| Project input | What we use it for | Format we work from |
|---|---|---|
| Part drawing with tolerances and datums | Pattern design, machining allowance, inspection strategy | 2D drawing with GD&T, or 3D model plus critical feature list |
| Material grade and standard | Melt chemistry, test frequency, certificate content | Grade designation with the governing standard |
| Annual volume and release pattern | Line selection, pattern quantity, tooling cost spread | Forecast with batch size and call-off rhythm |
| Machining and coating scope | Turning operations, surface preparation, coating thickness | Finished-part drawing with painted or bare areas marked |
| Acceptance requirements | Sample approval, NDT scope, dimensional report content | Inspection plan or written acceptance note |
| Packaging and delivery scope | Protection of machined faces, marking, crate layout | Packaging specification and destination |
Our ODM & OEM route runs through drawing confirmation and quotation, pattern making, sample submission, customer confirmation, mass production, inspection and shipment. Samples are always approved by the customer before volume casting begins.
Frequently Asked Questions
Which ductile iron grades do you cast for semiconductor accessories?
Grade comes from your drawing or is agreed during sampling. Ferritic and pearlitic nodular irons in roughly the 400 MPa to 700 MPa minimum tensile range, with elongation between about 2% and 18%, cover most bases, frames, housings and fixture pads. We confirm grade, matrix condition and test frequency in the quotation.
Do you machine and coat the castings, or supply them as cast?
As-cast, shot blasted, primed and painted conditions are all quoted. Turning is carried out on our CNC lathes and lathes. An automatic paint line and an electrophoretic coating line are in planning for parts that need tighter control of film thickness, and we confirm the available coating route for a specific part at quotation.
What part sizes and weights fit your molding lines?
Our boxless shot-press lines handle moulds up to 610 × 510 × 240 mm and 750 × 650 × 250 mm, which suits small fittings through medium bases and housings in volume production. A lost foam line for 100 kg to 1000 kg castings is under development for heavier frame and base structures.
How is consistency maintained across a production run?
Patterns, gating and process parameters are frozen after sample approval, melt chemistry is checked on the SPECTRO spectrometer, sand properties are tested with our sand laboratory equipment, and the IATF 16949:2016 system covers in-process checks. Finished parts are inspected against the approved plan before shipment.
What inspection evidence accompanies a delivery?
Depending on the agreed acceptance scope, we issue material certificates with tensile and hardness results, dimensional reports against the drawing, and magnetic particle or ultrasonic records where soundness testing is specified. Traceability marking links the parts to the heat.
What do you need from us to prepare a quotation?
Send the finished-part drawing, material grade and standard, annual volume with batch sizes, machining and coating scope, acceptance requirements, and packaging or destination notes. With those inputs we confirm the foundry route and return a quotation covering pattern, sample and production activity.
Longwan Machinery adheres to the corporate purpose of "High
quality, good reputation, customer priority, service precedence".
- Service
- ODM & OEM
- CAPACITIES
- Contact Infor.
- [email protected]
- +86-515-83658999
- +86-152 5109 2111
- Group 2, Dingxi Village, Caoyan Town, Dafeng District, Yancheng City, Jiangsu, China
Mobile QR Code
Copyright © 2024 Yancheng Longwan Machinery Co., Ltd.All Rights Reserved.
Powder By: 
OEM/ODM Ductile Cast Iron Semiconductor Accessories Foundry
