


 English
 русский
 Deutsch

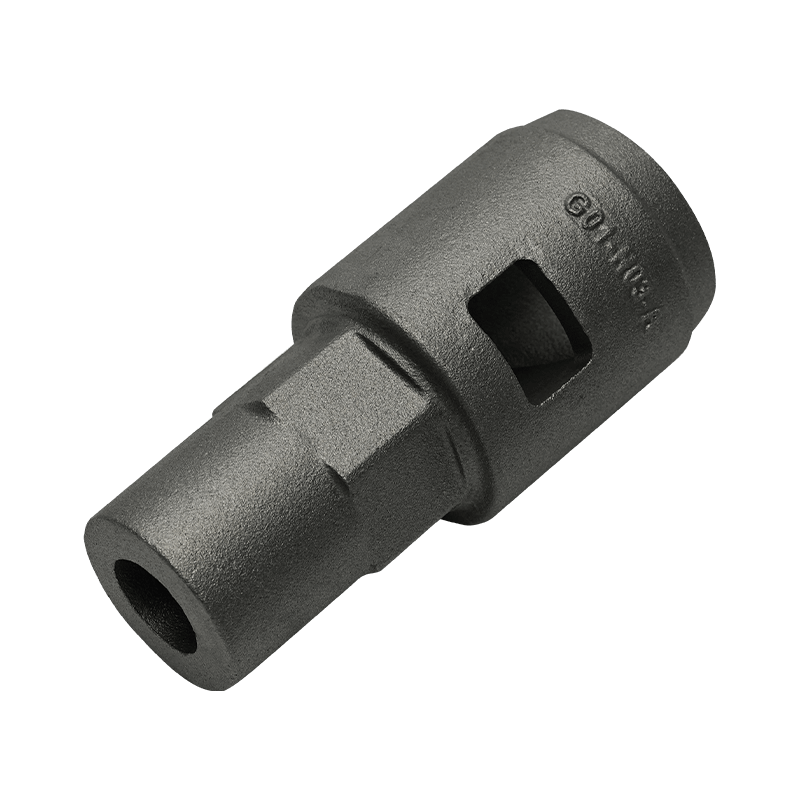
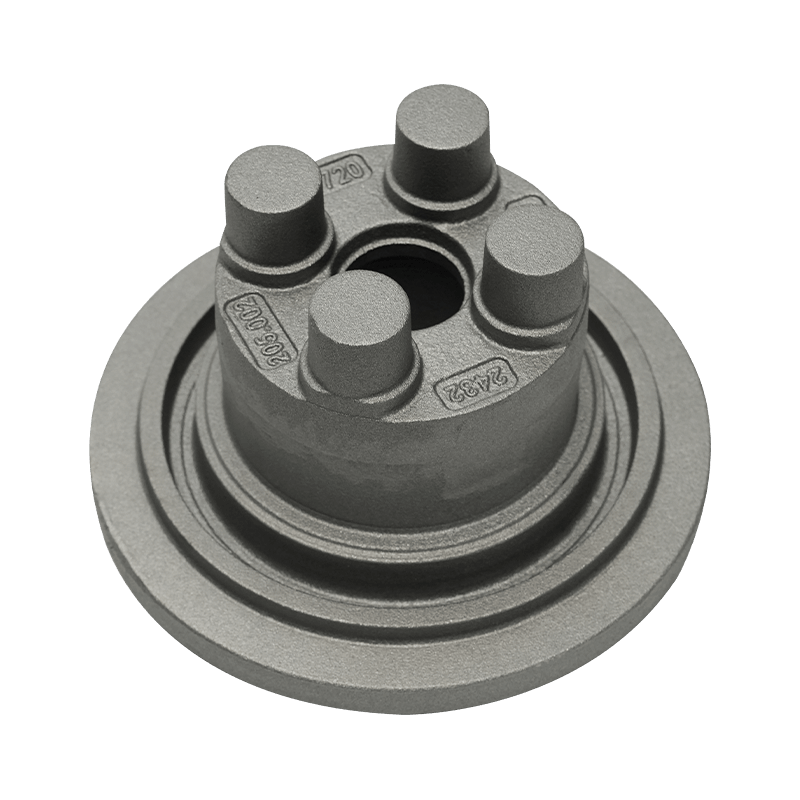
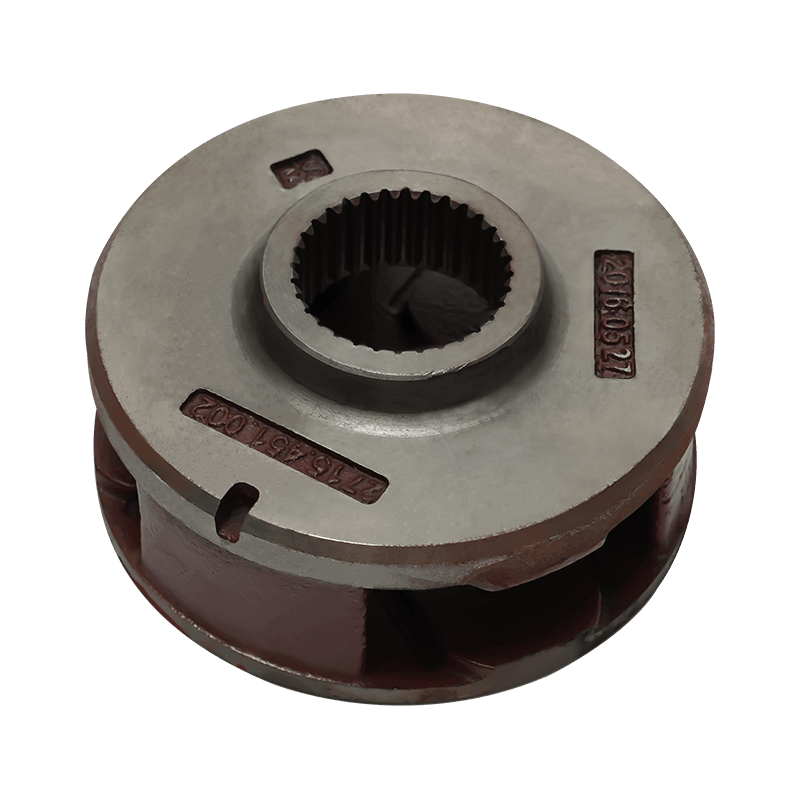
Grey Cast Iron Automotive Parts Foundry
Grey Cast Iron is a common cast iron material that is widely used in the manufacture of automotive parts. Grey cast iron is favored for its good wear resistance, heat resistance and good shock resistance. In automobile manufacturing, grey cast iron is often used to manufacture high-load parts such as brake discs. Its good thermal conductivity and fatigue resistance make it perform well in the braking system. Grey cast iron is also commonly used in the manufacture of components such as engine blocks and cylinder heads. Its stable material properties and reliable mechanical properties provide important support for the safety and reliability of the entire vehicle.
ABOUT US
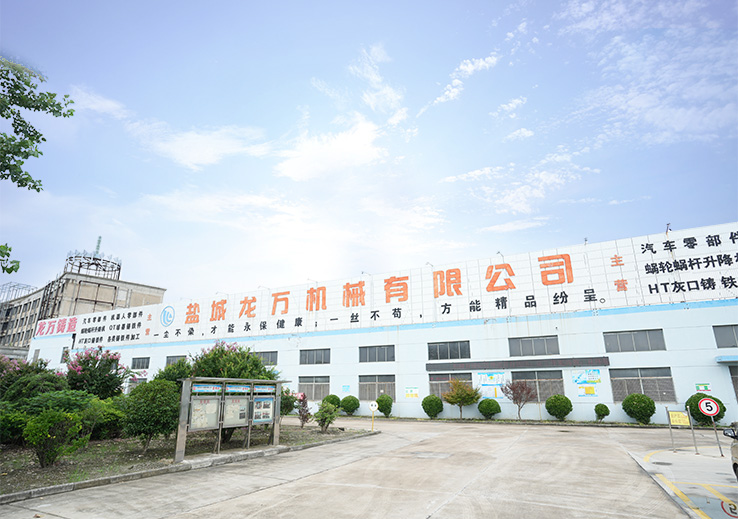
Yancheng Longwan Machinery Co., Ltd.
Founded in 2006, which located next to National Highway 204 in Yancheng City, Jiangsu Province, 40km from the center of Yancheng City, 5km from the center of Dongtai City, 30km from Dafeng District, and 10km from the exit of Baiju Expressway, with convenient transportation.
We mainly produce various types of fire-fighting pipe fittings, reducer parts, auto parts, agricultural machinery, and industrial robot parts. Its main customers include SAIC Group, Deere, Bonfiglioli (China), Shanghai Beixu, Yaskawa Electric, etc.
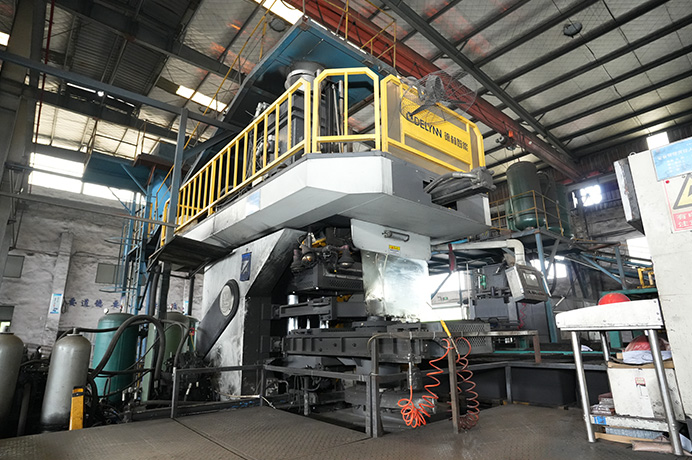
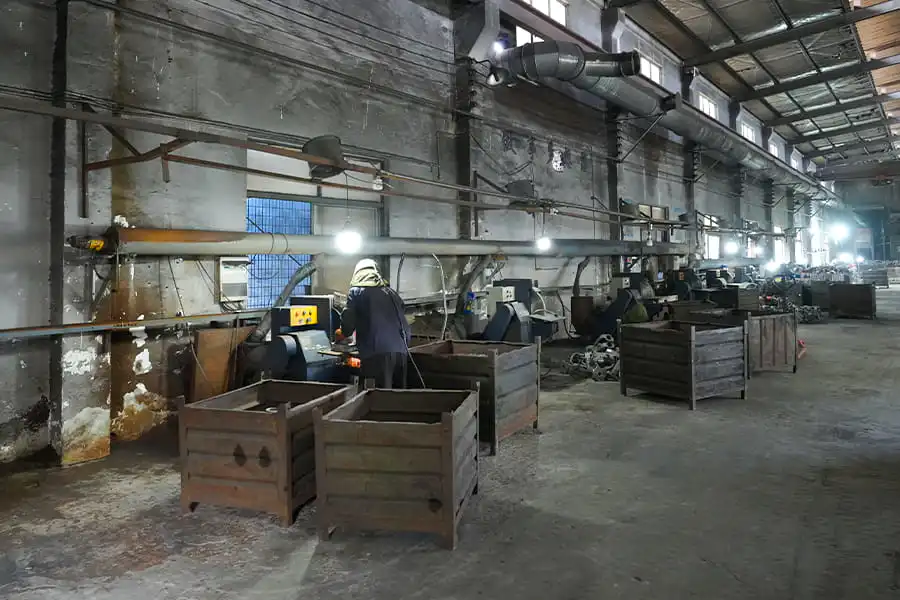
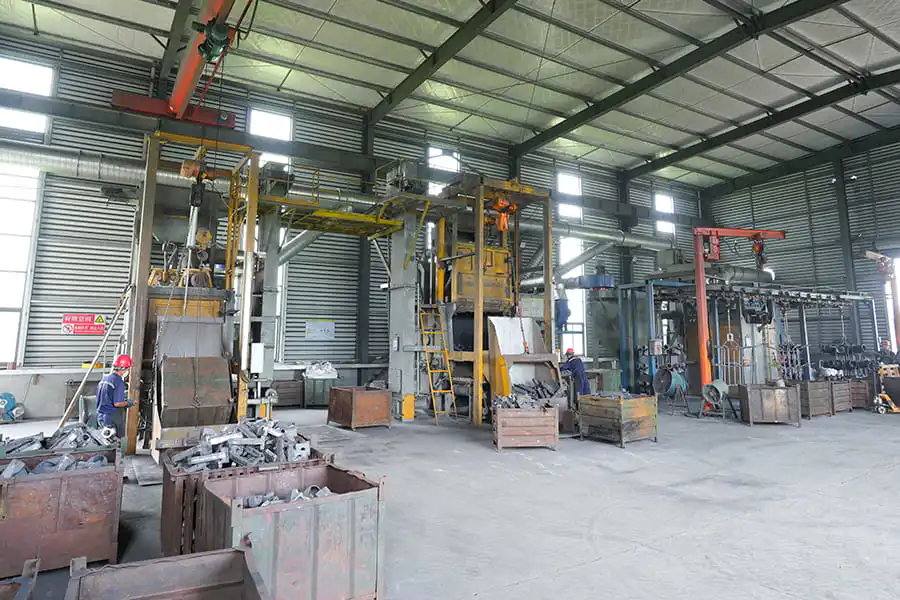
As a famous China Grey Cast Iron Automotive Parts Foundry and Grey Cast Iron Automotive Parts Suppliers, our company has a variety of molding equipment, including one vertical sand-shot horizontal parting boxless shot-press molding line with specifications of 610*510*240, 120 boxes/hour, suitable for mass production of small parts; one upper and lower sand-shot horizontal parting boxless shot-press molding line with specifications of 750*650*250, 100 boxes/hour, suitable for mass production of small and medium-sized parts; 3 sets of 1.25T medium-frequency electric furnaces; 3 cleaning shot blasting machines, and now planning a lost foam production line, suitable for 100Kg~1000Kg casting production, and planning an automatic spray painting line and an electrophoretic coating line at the same time, 3 CNC lathes and 3 lathes.
ODM Customization Expert
Advanced Production & Processing Equipment
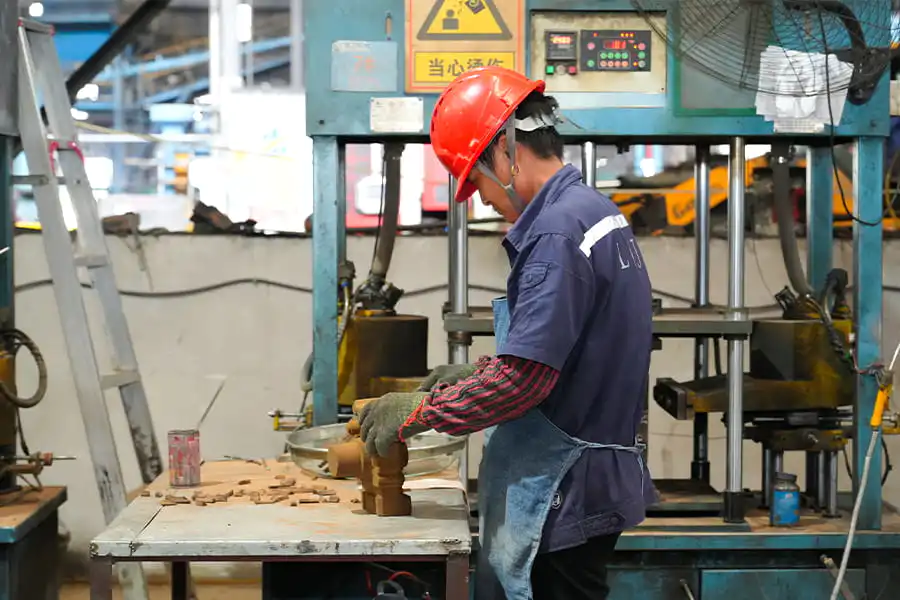
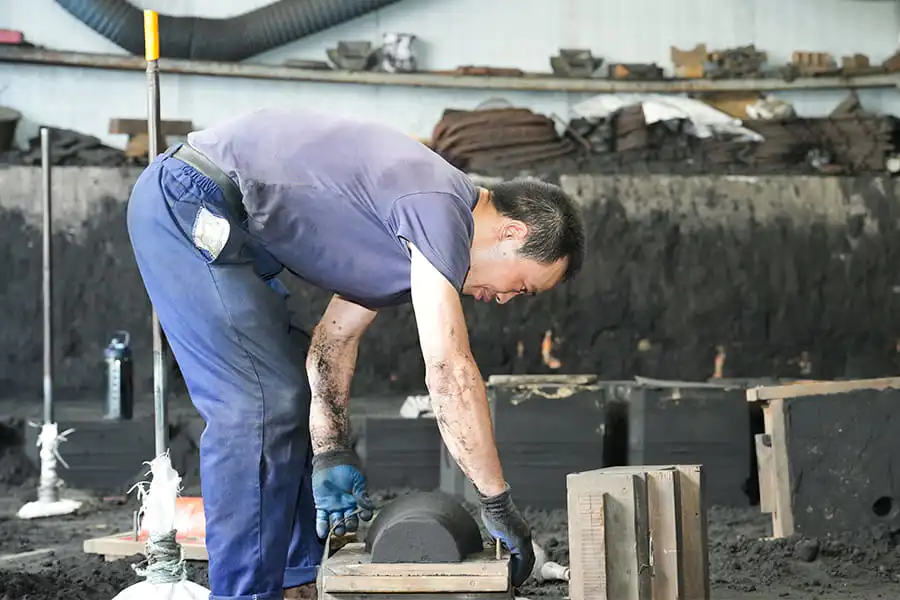
Longwan Machinery has a variety of advanced domestic and foreign molding equipment, including 2 fully automatic production lines for clay sand, 1 semi-automatic production line for clay sand, and 1 coated sand production line, with an annual production capacity of 15,000 tons.
Complete Inspection Flow
Strict Quality Inspection
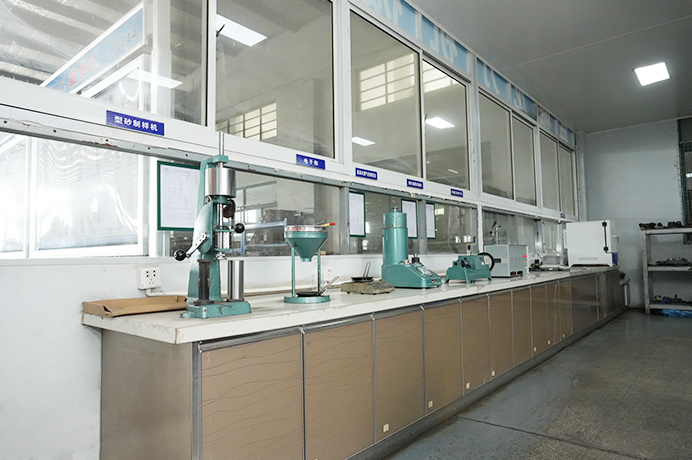
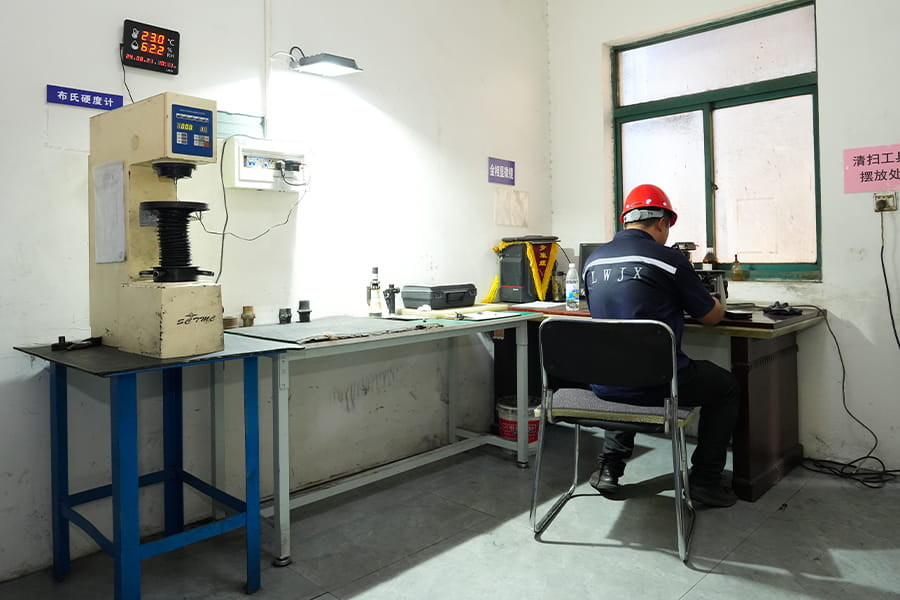
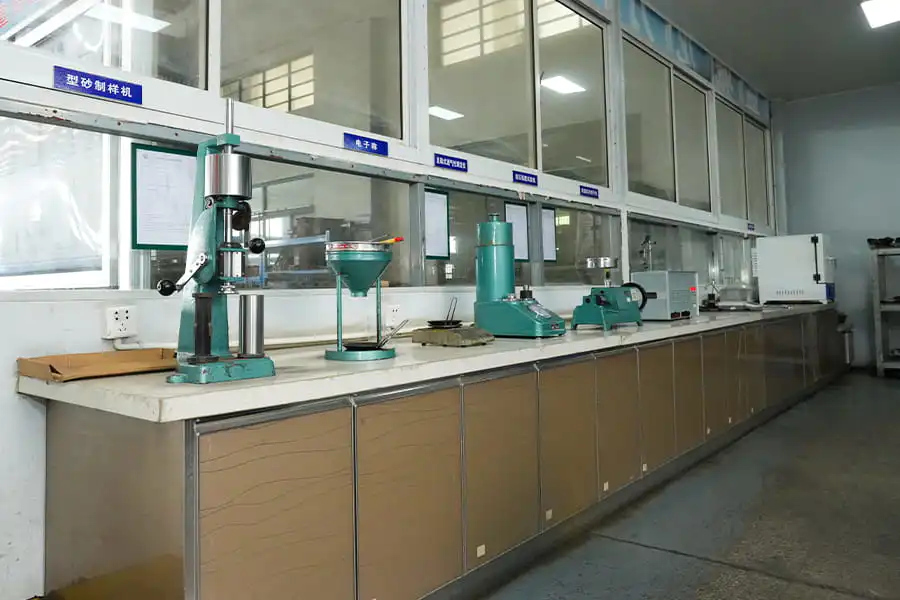
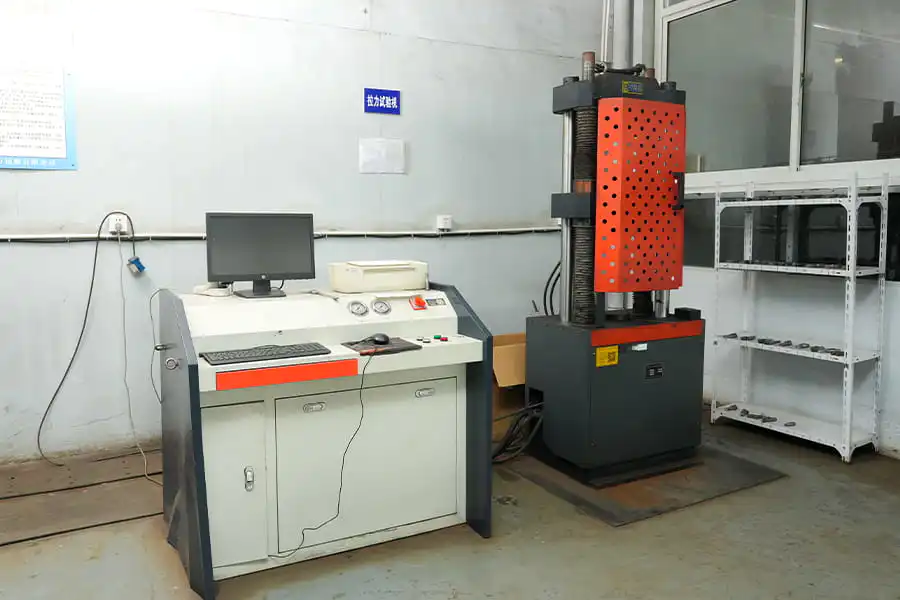
We have full-process testing equipment: spectrum analyzer, metallographic microscope, universal tensile testing machine, magnetic particle flaw detector, ultrasonic flaw detector, etc.
The above equipment can fully ensure that we can provide customers with high-precision final castings, and at the same time ensure that we meet customers' comprehensive testing requirements for physical and chemical properties of materials, non-destructive testing, high-precision geometric dimension testing, etc.
Professional Casting Expert
Comprehensive Casting Manufacturer
FAQ
-
QWhere are your products mainly exported to?A
Our products are mainly exported to multiple countries such as Germany, Japan, Italy, South Korea, and Australia.
-
QHow to deliver the goods to us?A
Usually, we ship by sea, which is very convenient for export.
Of course, if the customer's goods are urgent, we can also air freight them. Ningbo Airport and Shanghai International Airport are both very close to us.
-
QWhat's the payment term?A
When quoting, we will confirm the transaction method with you.
For mass production, we usually make a 50% advance payment in advance and then inspect and confirm the shipment before paying the remaining balance.
-
QHow to guarantee the quality of your goods?A
Firstly, there will be corresponding inspections after each process, and for the final completed product, we will conduct a full inspection according to customer requirements and international standards;
Then, we have advanced and complete top testing equipment in the industry: spectral analyzers, metallographic microscopes, universal tensile testing machines, magnetic particle testing machines, ultrasonic testing machines, etc.
The above equipment can fully ensure the provision of high-precision final castings to customers, while also meeting the comprehensive testing requirements of customers for material physical and chemical properties, non-destructive testing, high-precision geometric dimension testing, and so on.
-
QHow many employees of your company? what about the technicists?A
Our company has more than 120 employees, including 10 professional technicians and 5 engineers.
-
QHow about the capacity of your company?A
We have 2 fully automatic clay sand production lines, 1 semi-automatic clay sand production line, and 1 coated sand production line, with an annual production capacity of 15000 tons.
-
QDo you have some standard parts?A
No, currently we produce and customize according to the requirements based on the drawings provided by the customer.
-
QCan you do customized products?A
Yes, we are mainly doing customized products according to the customers’ drawings or samples.
-
QWhat applications do your products relate to?A
Our products cover almost all the applicable equipment manufacturing and machinery manufacturing and processing fields, mainly including automotive trucks, engineering machinery, agricultural machinery, reducers, water pumps, water treatment systems, and other fields.
-
Qwhat products can you offer?A
We mainly produce cast iron parts made of gray cast iron and ductile iron materials.
-
QAre you a direct manufacturer or trading company?A
We are a foundry and a manufacturer of cast iron parts.
-
QHow long can I get the feedbacks after we sent the inquiry?A
We will reply to you within 24 hours of the working day.
NEWS
-
How Is Grey Cast Iron Made? A Foundry's Step-by-Step Guide to Sand Casting
Grey cast iron has been poured into sand moulds for centuries, yet the questions buyers ask have barely changed: what actually goes into the furnace,...
READ MORE -
How Many Types of Cast Iron Are There? Four Main Types and Two Extended Families
Ask a room full of foundry engineers how many types of cast iron are there, and you will usually hear two numbers: four, or six. Both answers are cor...
READ MORE -
How Does Carbon Affect Steel? Understanding Strength, Hardness & Ductility
Carbon is the single most influential alloying element in steel. A shift of just a few tenths of a percent can turn a soft, bendable sheet into a har...
READ MORE -
How Is Ductile Iron Pipe Made? Inside the Foundry Process Step by Step
Ductile iron pipe has served as a backbone of modern water systems for decades. Engineers choose it because it combines pressure capacity, impact res...
READ MORE
Grey Cast Iron Automotive Parts Industry knowledge
Yancheng Longwan Machinery Co., Ltd. operates as a Grey Cast Iron Automotive Parts manufacturer in Dafeng District, Yancheng City, Jiangsu Province, producing OEM and ODM automotive castings from customer drawings and samples. The automotive programme runs alongside reducer parts, fire-fighting pipe fittings, agricultural machinery and industrial robot parts, with castings supplied into volume programmes for customers including SAIC Group, Deere, Bonfiglioli (China), Shanghai Beixu and Yaskawa Electric.
The range is built for parts that carry load, dissipate friction heat or damp vibration in service: braking components, engine and cylinder group parts, driveline housings and brackets. Castings leave our plant either as-cast, shot blasted, or cast and machined, depending on how the drawing defines the finished part.
What We Supply in This Range
Grey cast iron is specified for automotive parts where graphite-flake structure matters more than elongation. We pour and finish those parts to the casting drawing, and quote the machining scope separately from the foundry scope.
- Braking components — brake discs and rotors, brake drums, backing plates. Graphite flakes raise thermal conductivity and give a self-lubricating effect at the friction surface.
- Engine and cylinder group — engine blocks, cylinder heads, cylinder liners, flywheels, where compressive strength and heat dissipation suit continuous thermal cycling.
- Driveline and transmission — clutch parts, bearing caps, cover plates, differential and gearbox housings.
- Manifold, pump and bracket parts — exhaust manifolds, water pump bodies, mounting brackets, where damping and machinability outweigh the need for high tensile elongation.
Parts that need higher tensile strength or impact elongation rather than damping are normally placed on our ductile cast iron automotive parts route instead. Heavier grey iron housings outside the automotive set follow the same material and molding approach as our grey cast iron reducer accessories.
Grey Iron Grades and Where Each One Fits
Grade is set by the drawing, not by us. Castings are poured to the designation named on the customer specification — EN 1561 GJL series, ASTM A48 classes, JIS G5501 FC series or GB/T 9439 HT series — with composition adjusted through furnace charge and inoculation, and grade confirmed on separately cast test bars.
| Designation family | Typical automotive use | What we verify |
|---|---|---|
| GJL-150 / A48 Class 20 / FC150 / HT150 | Covers, low-stress housings, brackets | Composition, hardness, casting soundness |
| GJL-200 / A48 Class 25–30 / FC200 / HT200 | Brake drums, pump bodies, bearing caps | Tensile test bar, Brinell hardness, graphite form |
| GJL-250 / A48 Class 35 / FC250 / HT250 | Brake discs and rotors, flywheels, cylinder liners | Tensile test bar, hardness, microstructure, dimensions |
| GJL-300 / A48 Class 40 / FC300 / HT300 | Engine blocks, cylinder heads | Composition control, microstructure, casting integrity, NDT where specified |
Raising tensile strength in grey iron reduces damping and thermal conductivity, so the grade named on a vehicle programme drawing is normally the grade the programme has already validated. We confirm that we can reach it rather than substituting something else. For grades outside the four bands above, our grey cast iron range and melt shop set the practical limits, and we say so during quotation.
Molding Lines and Annual Capacity
Two fully automatic clay sand lines, one semi-automatic clay sand line and one coated sand line give an annual casting capacity of 15,000 tonnes, backed by three 1.25 T medium-frequency electric furnaces and three cleaning shot blasting machines.
| Equipment | Key specification | What it suits |
|---|---|---|
| Vertical sand-shot, horizontal parting boxless shot-press line | 610 × 510 × 240 mm, 120 boxes/hour | High-volume small automotive parts |
| Upper and lower sand-shot, horizontal parting boxless shot-press line | 750 × 650 × 250 mm, 100 boxes/hour | High-volume small and medium parts |
| Clay sand lines | 2 automatic, 1 semi-automatic | Serial production plus larger pattern work |
| Coated sand line | Coated sand moulds and cores | Cores and parts needing tighter surface and dimensional control |
| Machining | 3 CNC lathes, 3 lathes | Turning of cast-and-machined parts |
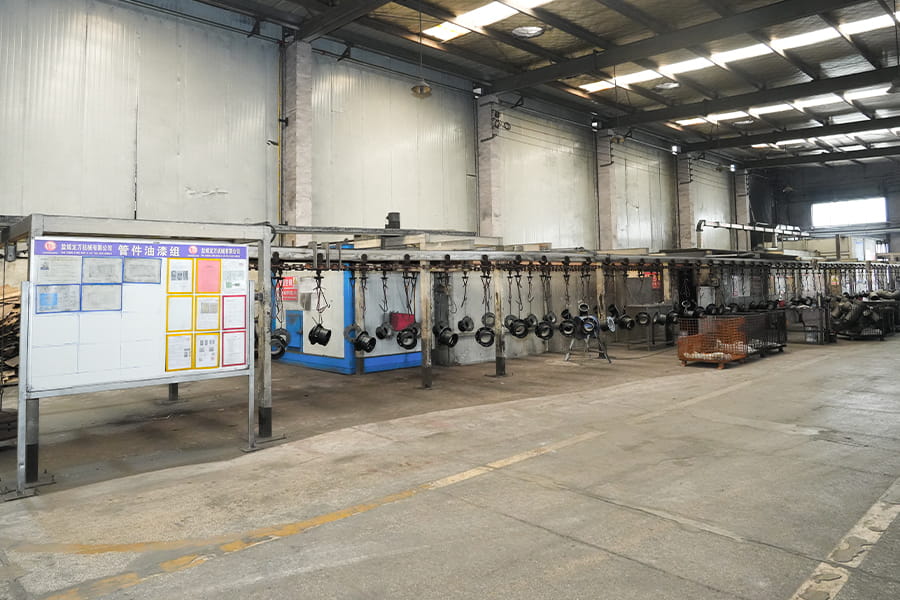
| Planned expansions | Lost foam line for 100–1000 kg castings; automatic spray painting and electrophoretic coating lines | Heavier castings and in-house finishing |
Lost foam and the paint and electrophoretic coating lines are formal expansion plans rather than current production. Where a programme depends on them, we confirm availability against your timing during quotation and keep the route on the process sheet.
Application Fit in Vehicle Systems
Grey iron behaves differently in each vehicle system, and the casting design follows that behaviour rather than a generic material preference.
Braking
Discs and drums work under friction heat and repeated mechanical load. Graphite flakes improve thermal conductivity and provide a self-lubricating effect at the friction surface, while the flake structure absorbs vibration instead of passing it into the suspension. The parameters we hold on the casting side are graphite form, hardness and freedom from porosity or shrinkage in the working section.
Engine and cylinder group
Blocks, heads and liners combine compressive load with sustained thermal cycling. Cylinder liners use graphite for oil retention and wear resistance; blocks and heads rely on damping and heat transfer more than on tensile strength. Wall thickness, core stability and cooling rate through the casting decide whether the specified grade is reached in the section that matters.
Driveline, housings and brackets
Clutch parts, gearbox and differential housings, bearing caps and cover plates benefit mainly from damping and machinability. Reduced transmission of gear noise and stable machined faces are usually the acceptance drivers rather than strength.
Machining, Finishing and Line Integration
Machining scope is fixed at quotation: which faces, bores, registers and threads are produced by us, and which features remain as-cast. Draft angle, parting line and core print position are agreed before pattern making, because they set the dimensional margin available for the finished part.
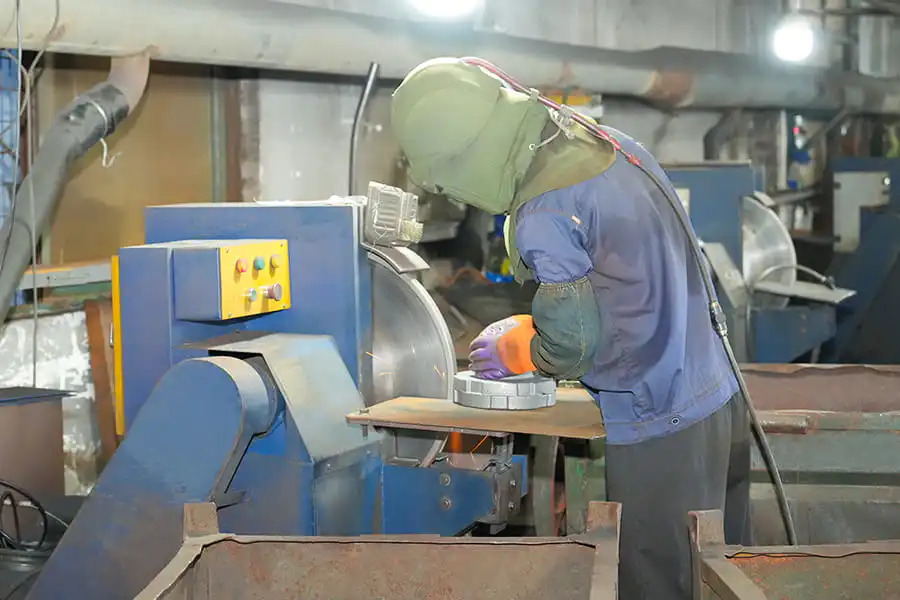
- Turning — OD and ID turning, facing and grooving on three CNC lathes and three lathes.
- Surface preparation — shot blasting on three cleaning machines removes sand and scale before machining or coating.
- Coating — corrosion protection is agreed per project; the automatic spray painting and electrophoretic coating lines are planned.
- Assembly-side features — registers, bolt patterns and seal grooves are confirmed at drawing review so parts seat correctly in your fixture or line.
- Marking and traceability — marking content and record level are agreed before serial delivery.
Inspection and Acceptance Testing
Longwan Machinery holds an IATF 16949:2016 system standard and inspects through the entire process: random checks on incoming material, in-process control against defects, and final inspection of finished parts before shipment.
| Check | Equipment or method | Stage |
|---|---|---|
| Chemical composition | German SPECTRO direct-reading spectrometer | Each heat |
| Tensile strength | Tensile testing machine, separately cast test bars | Per cast or lot |
| Hardness | 3T Brinell hardness tester | Per batch and per sample |
| Microstructure and graphite form | Metallographic microscope; sonic velocity meter for batch comparison | Process verification and grade confirmation |
| Surface and internal discontinuities | Magnetic particle flaw detector, ultrasonic flaw detector | When specified on the drawing or inspection plan |
| Molding sand properties | SAC hammer-type sample making machine, SWY hydraulic strength testing machine, SSZ vibration-type sand screening machine, SGS double-disc infrared dryer | Daily, before and during production |
| Dimensional conformity | Drawing tolerances, agreed gauges and fixtures, high-precision geometric dimension checks | First article, in-process and final |
Acceptance is agreed before production starts. We confirm which characteristics are checked internally, which are witnessed or reviewed by your inspector, and which records travel with the shipment.
Information We Use to Configure Your Solution
A quotation that survives into serial production starts from complete part data. These inputs let us set molding line, pattern, grade and machining scope without assuming anything.
- 2D drawing and 3D model at the correct revision, with finished-part datums
- Material grade and the standard it references — EN 1561, ASTM A48, JIS G5501, GB/T 9439 or an internal specification
- Casting weight, maximum section thickness and any handling limit
- Annual volume, batch size and call-off pattern
- Machining scope, stock allowance, surface finish and thread requirements
- Coating, painting or plating requirement
- Non-destructive testing, leak or pressure test where applicable
- Critical-to-function dimensions, balancing or runout limits
- Identification marking, traceability and documentation level
- Packaging format and destination, with any rust-preventive requirement
- Target timing for tooling, samples and first serial delivery
How volume and weight decide the route: small parts at high volume run on the 610 × 510 × 240 mm shot-press line; small and medium parts on the 750 × 650 × 250 mm line; heavier castings in the 100–1000 kg band are planned for the lost foam route.
From Drawing to Mass Production
- Drawing or sample review and quotation — material, molding route, machining scope, tooling and inspection plan are confirmed. Working-day inquiries receive a reply within 24 hours.
- Pattern and core box manufacture — released after tooling order confirmation.
- Sample castings — produced from the new tooling and sent for dimensional and material confirmation.
- Mass production — released on your written approval of the sample.
- Inspection — in-process control plus final inspection, with joint inspection by your representative as an option.
- Shipment — sea freight as standard and air freight when the schedule demands it, with Shanghai International Airport and Ningbo Airport both within reach of the plant.
Packaging, Documentation and Dispatch
We provide one-stop scope from pattern design through casting, material verification and after-sales follow-up, and packaging can be designed to your requirement. Parts are mainly exported to Germany, Japan, Italy, South Korea and Australia. Mass production orders are usually handled with a 50% advance payment, with the balance confirmed after inspection and before shipment.
For wear parts replaced in service, the reference for later production is the approved sample and its process record, which keeps repeat batches aligned with the original drawing.
Frequently Asked Questions
Do you produce standard grey iron automotive parts or only custom parts?
We produce to customer drawings or samples; there is no standard catalogue of automotive castings. Patterns and core boxes are made for the part, and the casting is quoted against the drawing revision you supply.
Which grey iron grades can you quote against?
We quote against the grade named on your drawing — EN 1561 GJL series, ASTM A48 classes, JIS G5501 FC series or GB/T 9439 HT series — and confirm the casting weight, section thickness and molding route that support it. Grade is verified on separately cast test bars, with hardness and microstructure checks through production.
What are your molding capacity and main production equipment?
Two fully automatic clay sand lines, one semi-automatic clay sand line and one coated sand line give 15,000 tonnes of annual casting capacity. Molding runs on a 610 × 510 × 240 mm shot-press line at 120 boxes/hour and a 750 × 650 × 250 mm line at 100 boxes/hour, fed by three 1.25 T medium-frequency electric furnaces and cleaned on three shot blasting machines.
What inspection records come with the castings?
Documentation is fixed at quotation. It normally includes results for the poured grade, hardness and dimensional checks, together with the packing list. The submission level your quality function needs is confirmed before serial delivery, and inspection can be carried out jointly with your representative.
How are tooling and samples handled?
Patterns or moulds are made after the tooling order is confirmed, sample castings are produced from that tooling and sent to you for confirmation, and mass production starts only after your approval. This is the same sequence we use for ODM and OEM projects across all our cast iron part families.
What do you need from us to prepare a quotation?
Send the drawing or sample, the material grade and referenced standard, casting weight and section thickness, annual volume and call-off pattern, machining and coating scope, any NDT requirement, packaging format, destination and target timing for samples and first delivery. With those inputs we can confirm molding route, tooling, inspection plan and price.
Longwan Machinery adheres to the corporate purpose of "High
quality, good reputation, customer priority, service precedence".
- Service
- ODM & OEM
- CAPACITIES
- Contact Infor.
- [email protected]
- +86-515-83658999
- +86-152 5109 2111
- Group 2, Dingxi Village, Caoyan Town, Dafeng District, Yancheng City, Jiangsu, China
Mobile QR Code
Copyright © 2024 Yancheng Longwan Machinery Co., Ltd.All Rights Reserved.
Powder By: 
OEM/ODM Grey Cast Iron Automotive Parts Foundry
